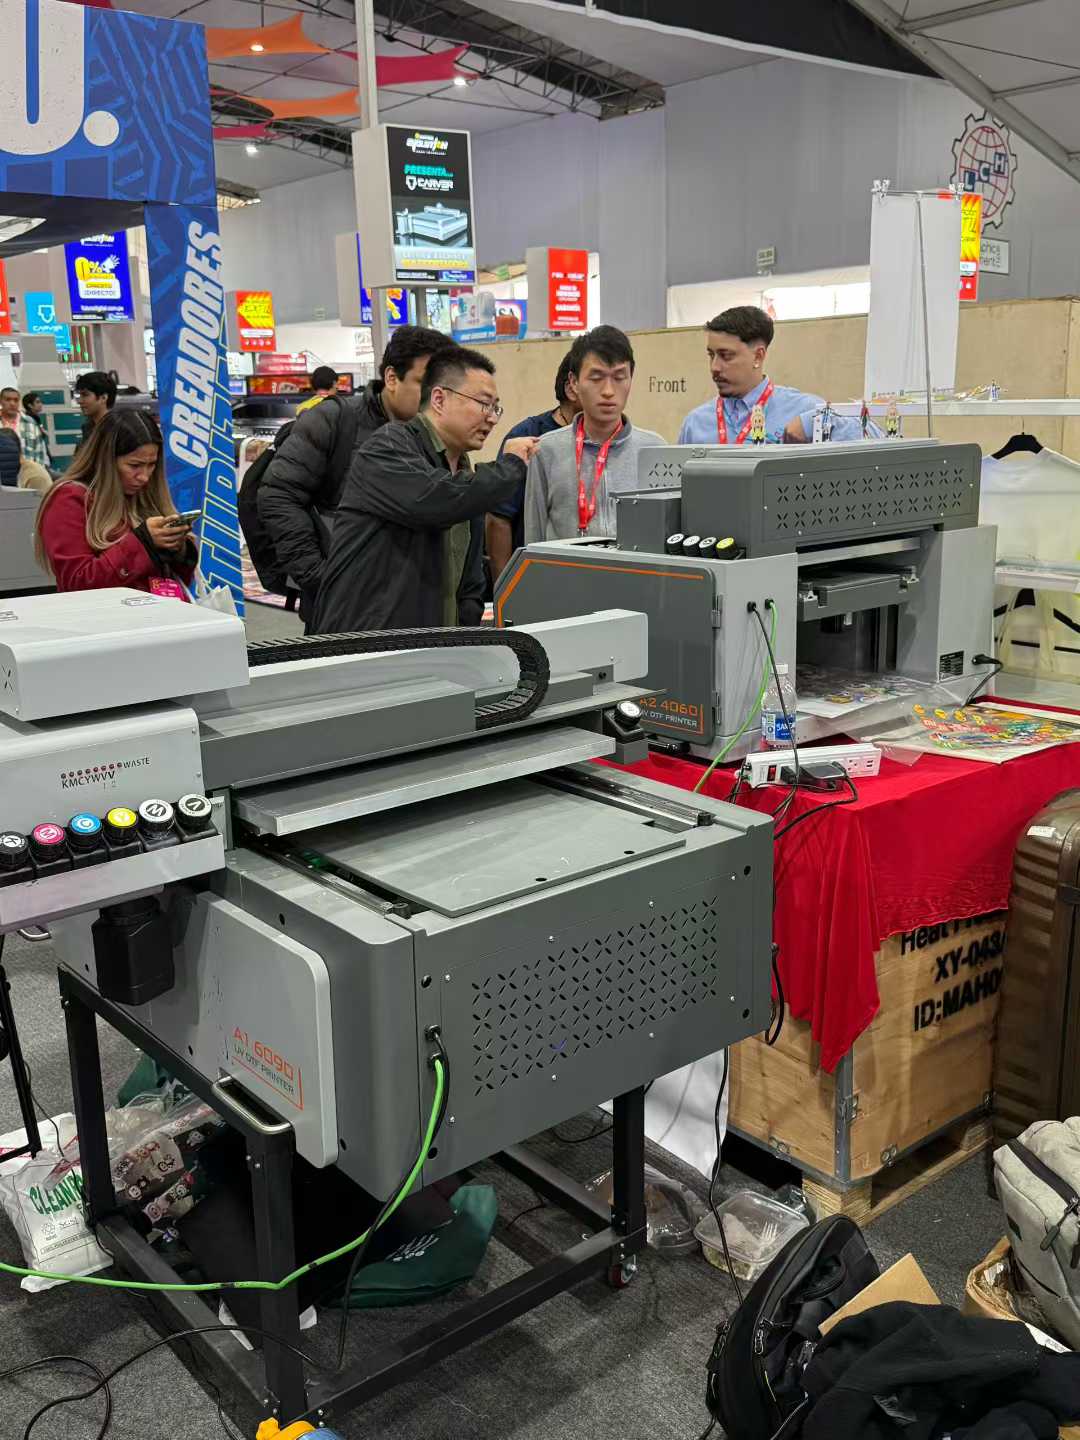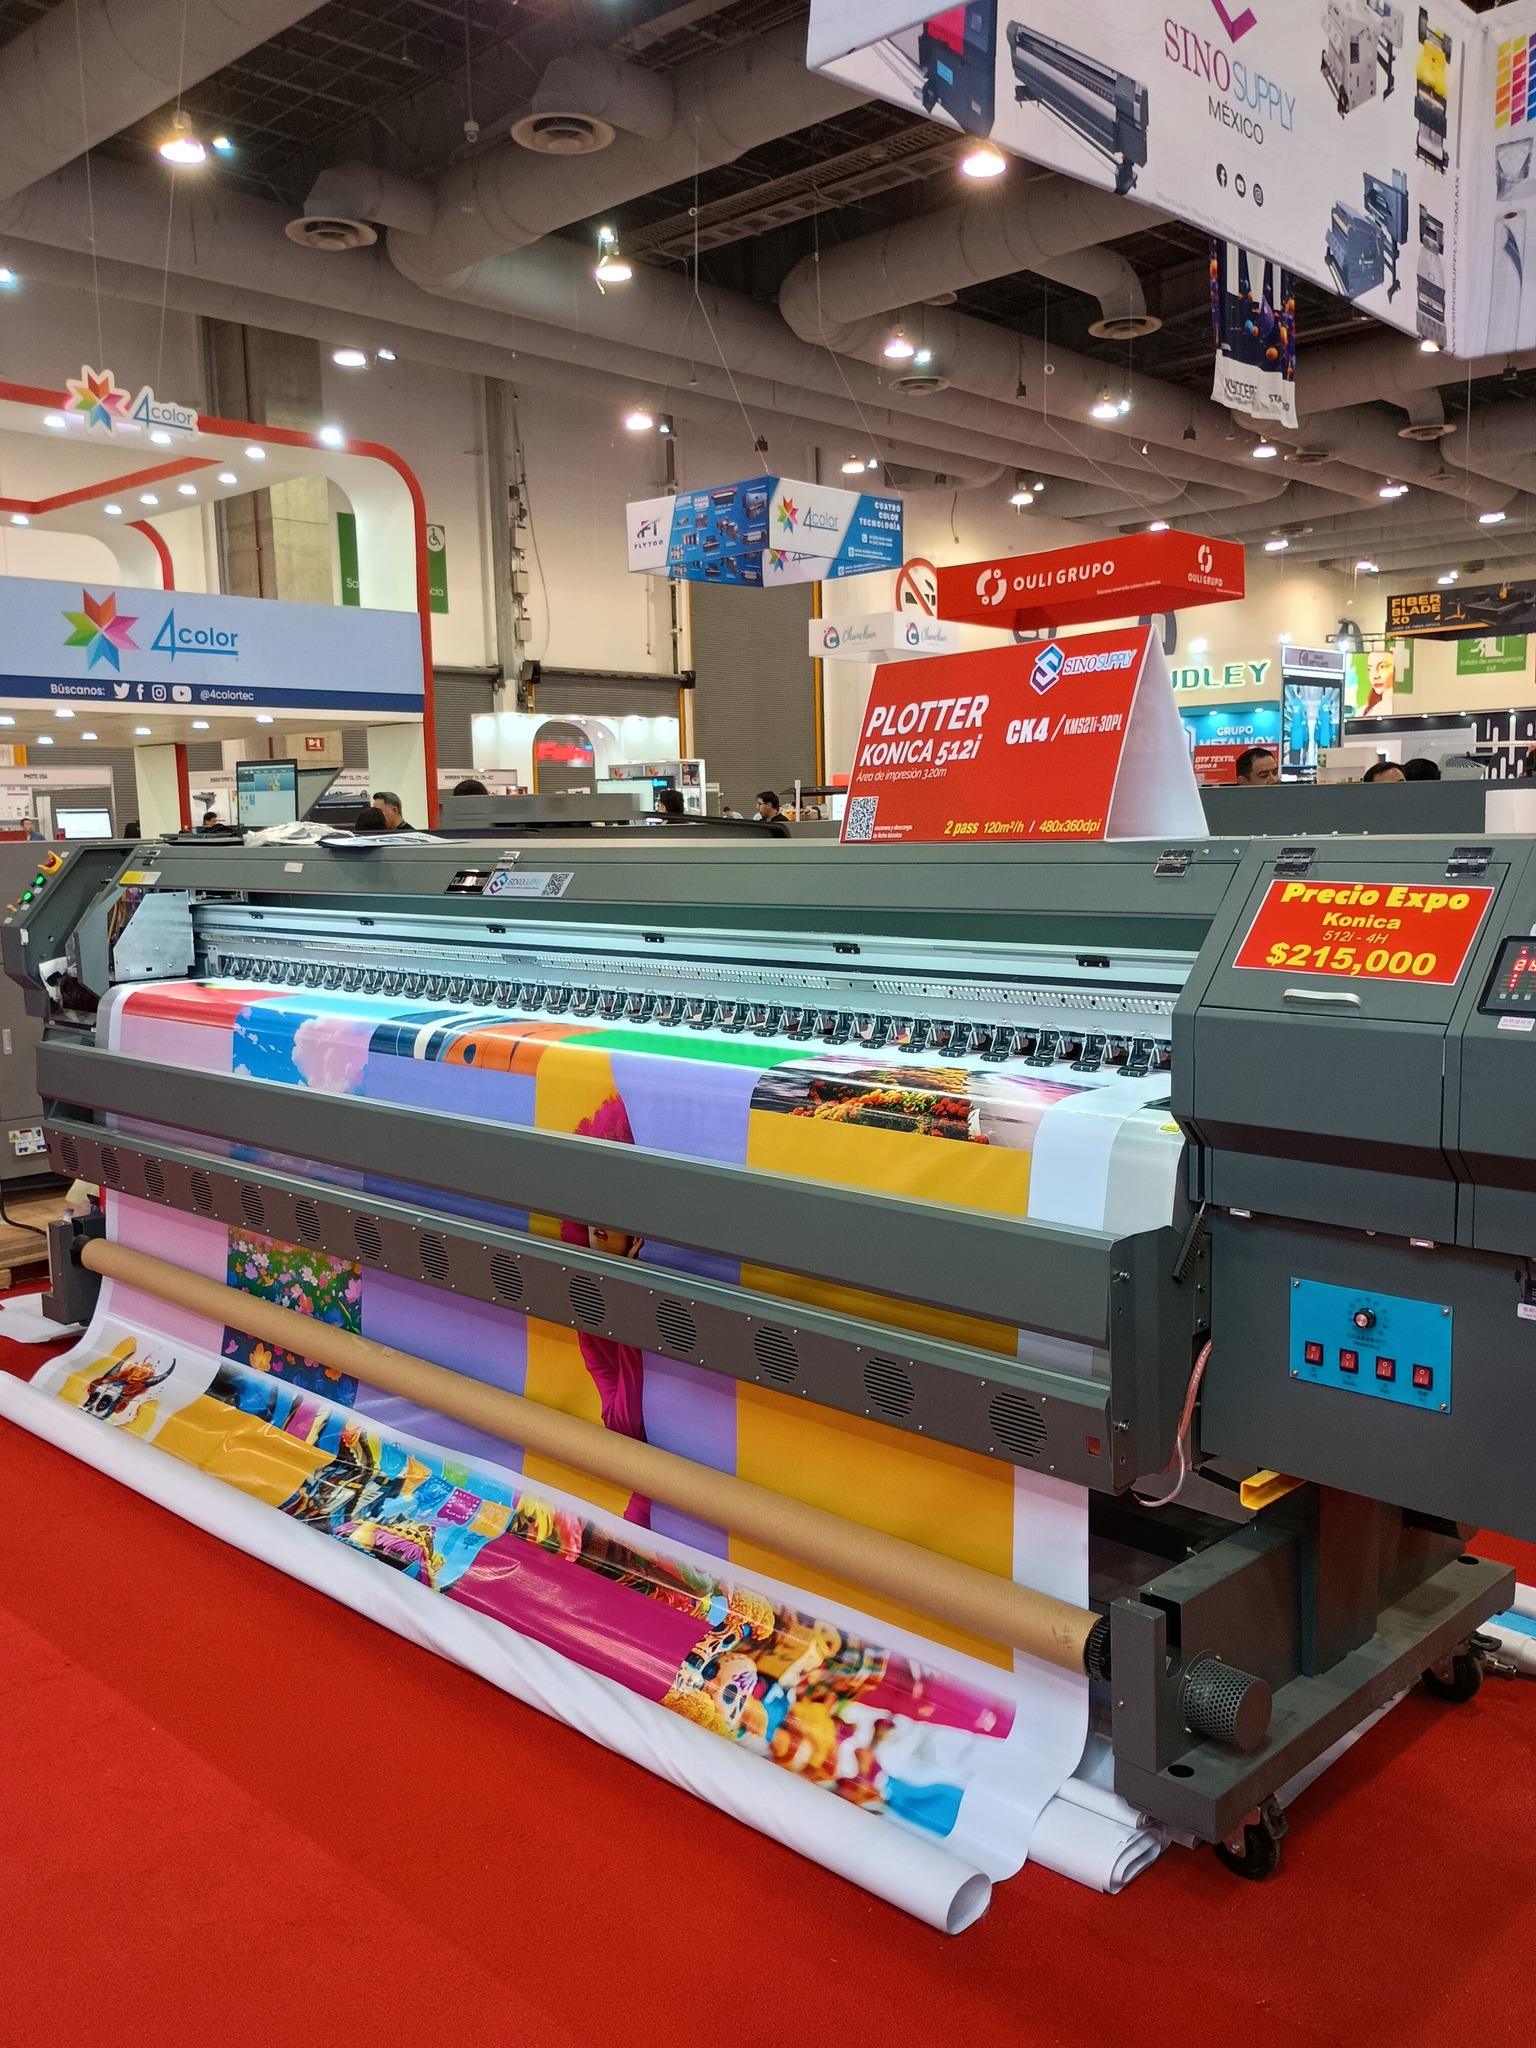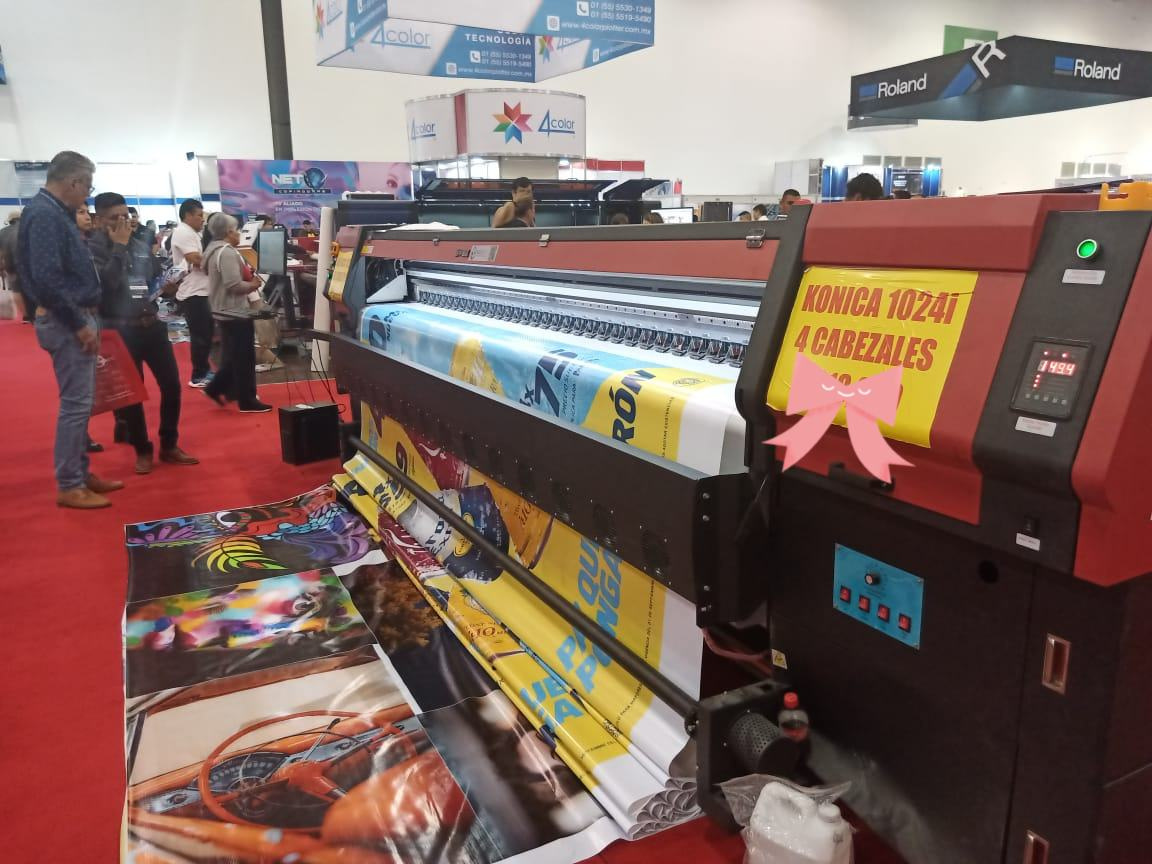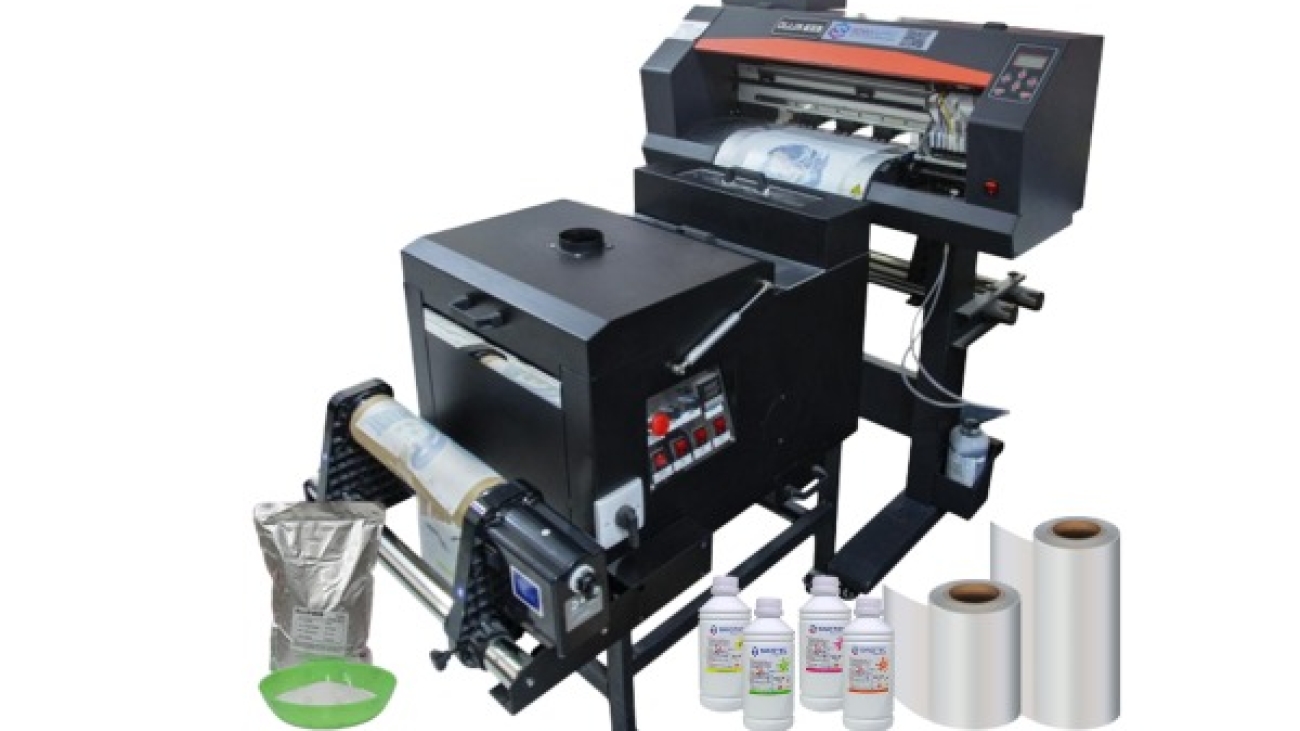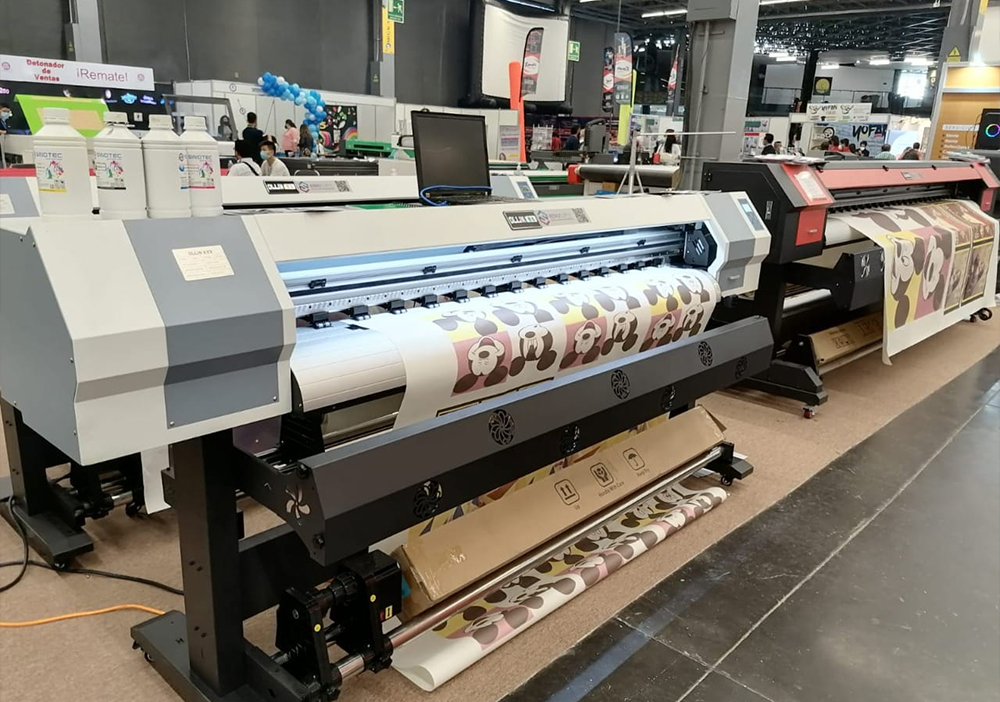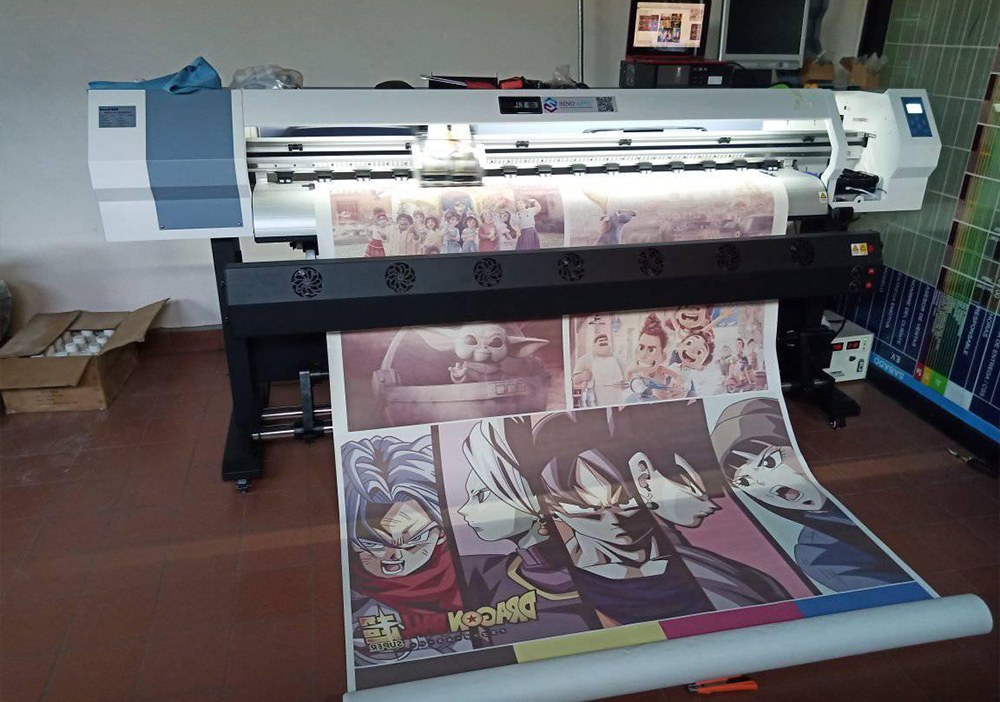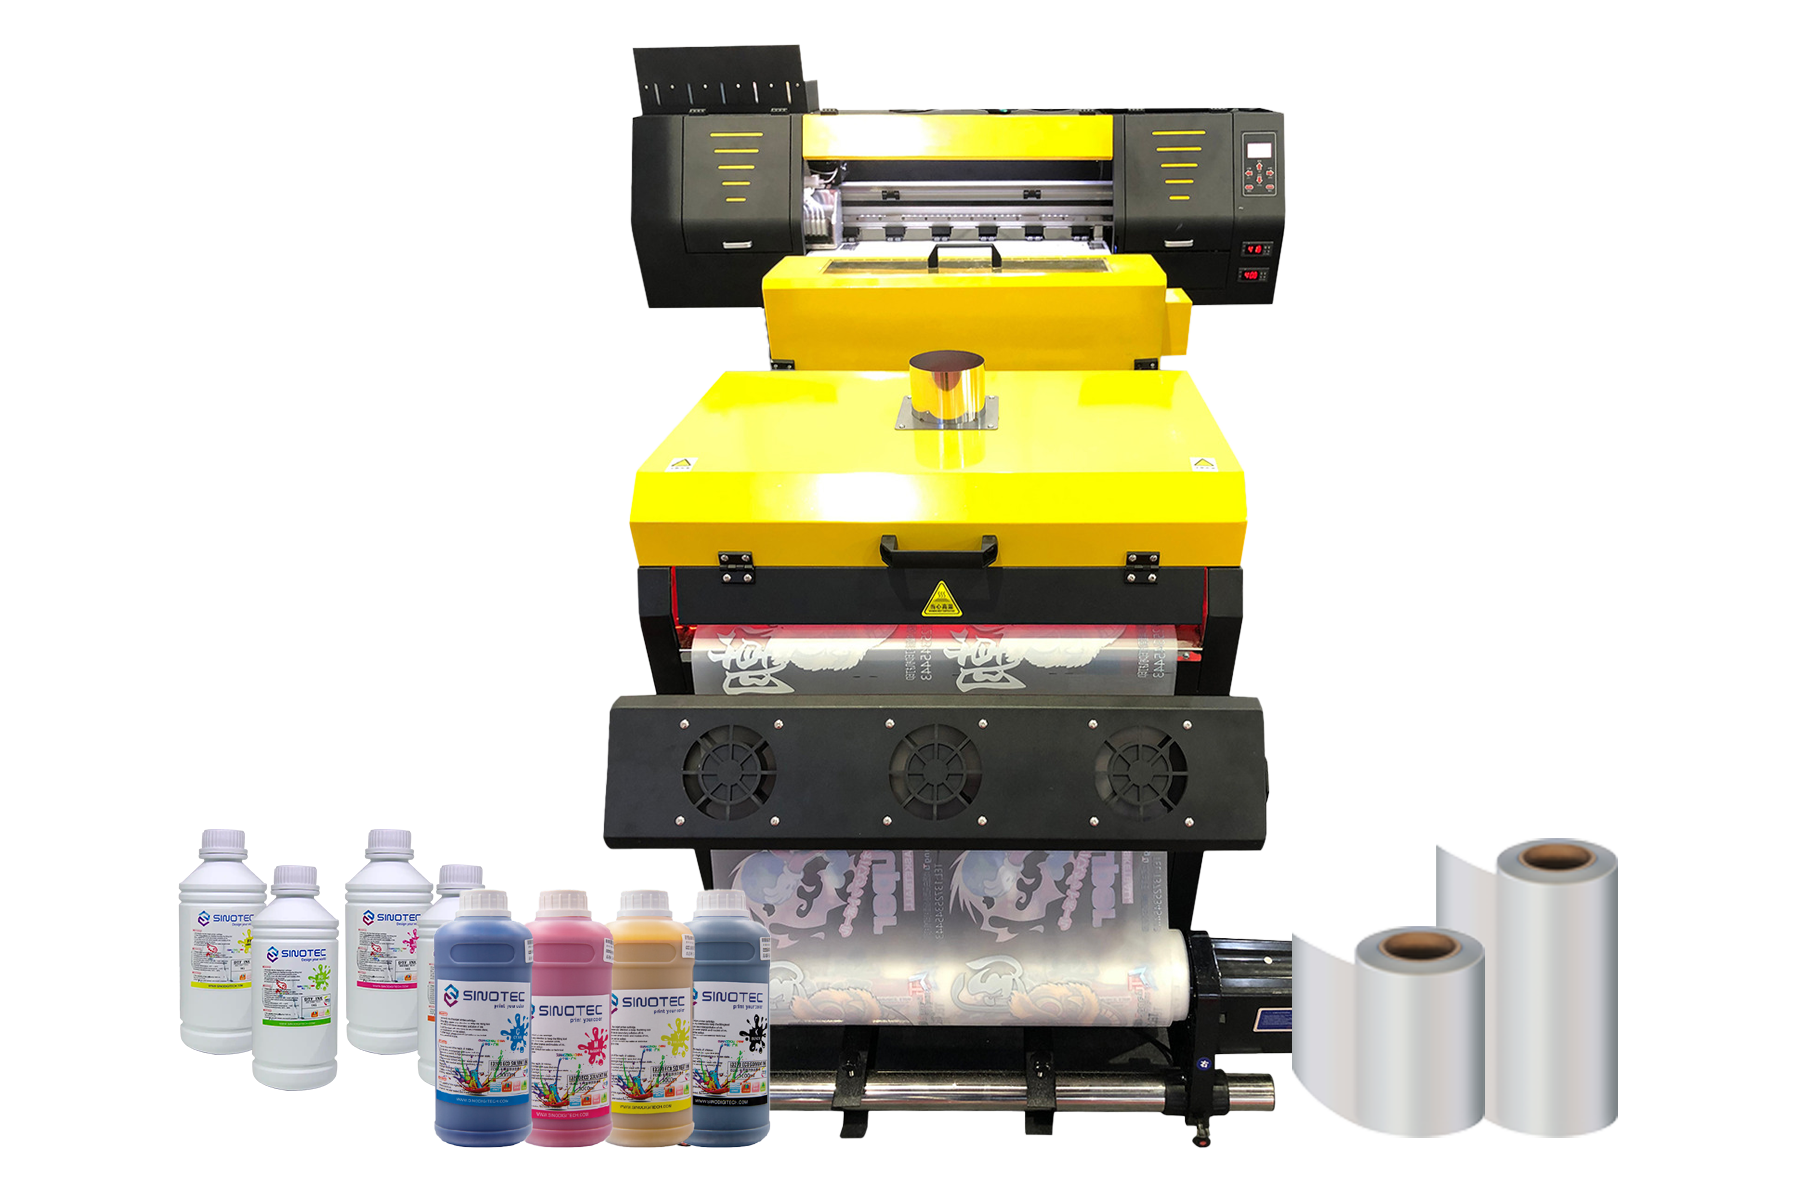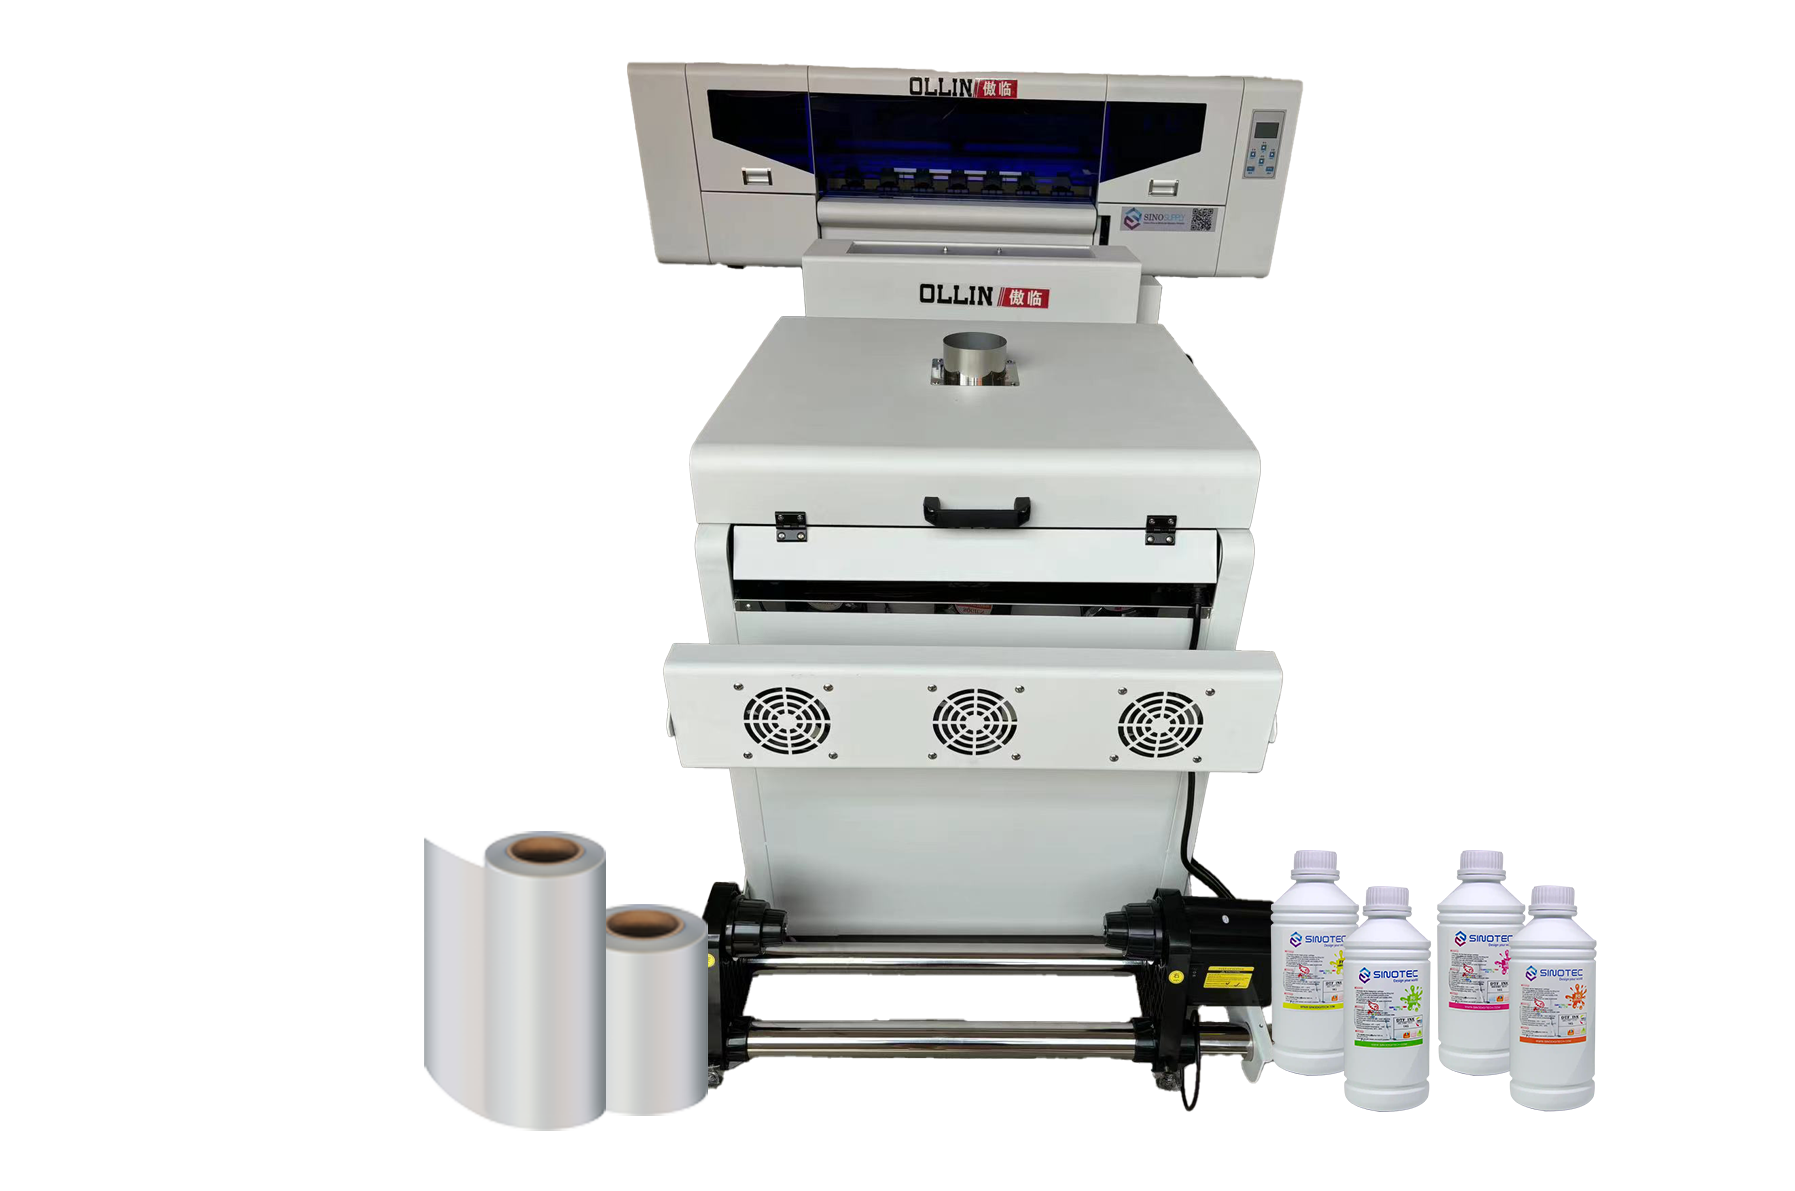
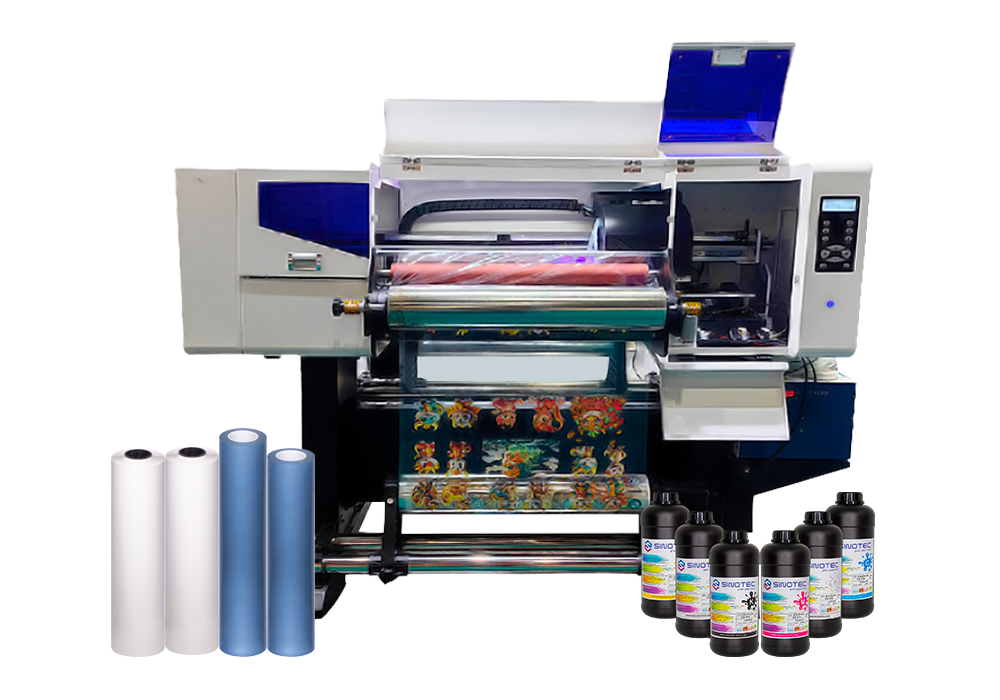
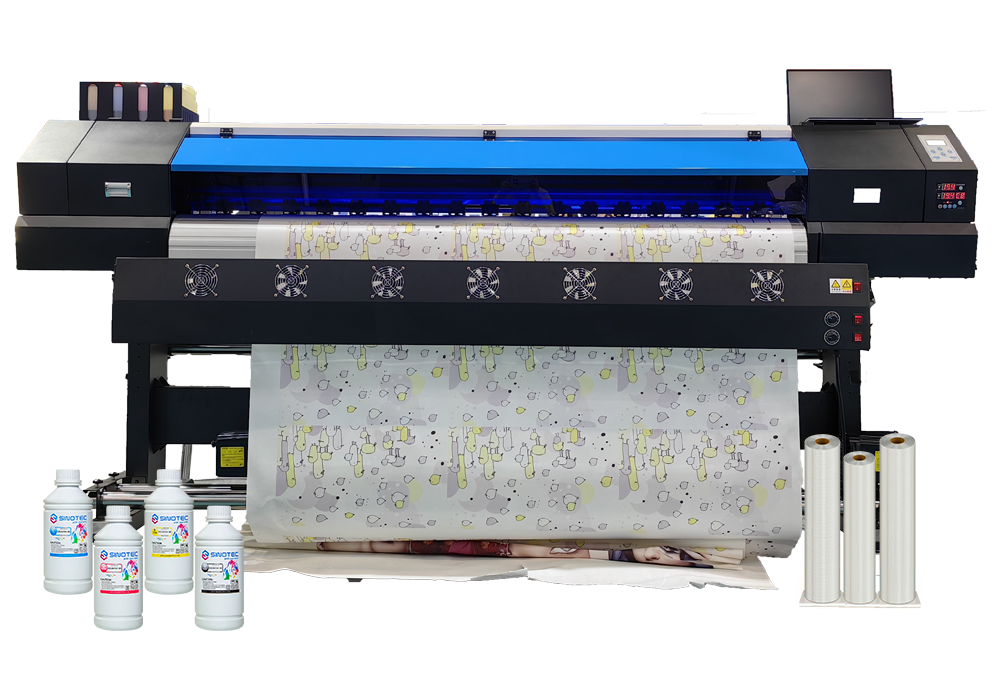
Máquina de impressão DTF

Lista de verificação de inicialização da máquina de impressão DTF: O que cada decisão de equipamento realmente afeta no downstream

Every equipment decision made at the procurement stage creates a chain of operational consequences that buyers often don’t fully account for until production is already underway. O DTF printing machine you select doesn’t just determine print quality — it shapes your ink consumption model, your pretreatment workflow, your curing equipment requirements, your staff training curve, and ultimately your per-unit cost structure. Getting this wrong early is expensive to correct later.

Print width is a good example of a decision that looks simple on a spec sheet but ripples downstream. A wider-format machine increases throughput per pass, which sounds like a win — but it also demands larger heat press equipment, more gang sheet planning discipline, and higher ink volume per job. Buyers sourcing for smaller custom order volumes sometimes default to a small DTF printer precisely because the operational footprint stays manageable and the capital outlay is lower, but they need to stress-test that choice against projected order growth before committing.

Ink system architecture is another area where the downstream effects are underestimated. White ink recirculation — or the absence of it — directly affects nozzle clogging frequency, maintenance intervals, and the true cost of machine downtime. UM desktop DTF printer designed for low-volume environments may handle intermittent use better than a mid-range machine that requires consistent daily throughput to keep ink channels clear. That’s a workflow constraint, not just a hardware spec.

Before finalizing any supplier conversation, procurement teams should map these interdependencies explicitly:

  • Print width vs. available heat press capacity and gang sheet workflow
  • Ink system type vs. expected daily print volume and maintenance staffing
  • Film feed mechanism vs. roll media compatibility and substrate flexibility
  • RIP software compatibility vs. existing design and prepress infrastructure
  • Power and ventilation requirements vs. facility readiness
  • OEM/ODM customization options vs. branded output requirements

Suppliers who support specification customization — adjusting configurations to match a buyer’s actual production environment rather than pushing a standard SKU — tend to reduce this downstream friction considerably. The checklist above isn’t exhaustive, but it reflects where most procurement decisions create unintended operational costs when left unexamined at the sourcing stage.
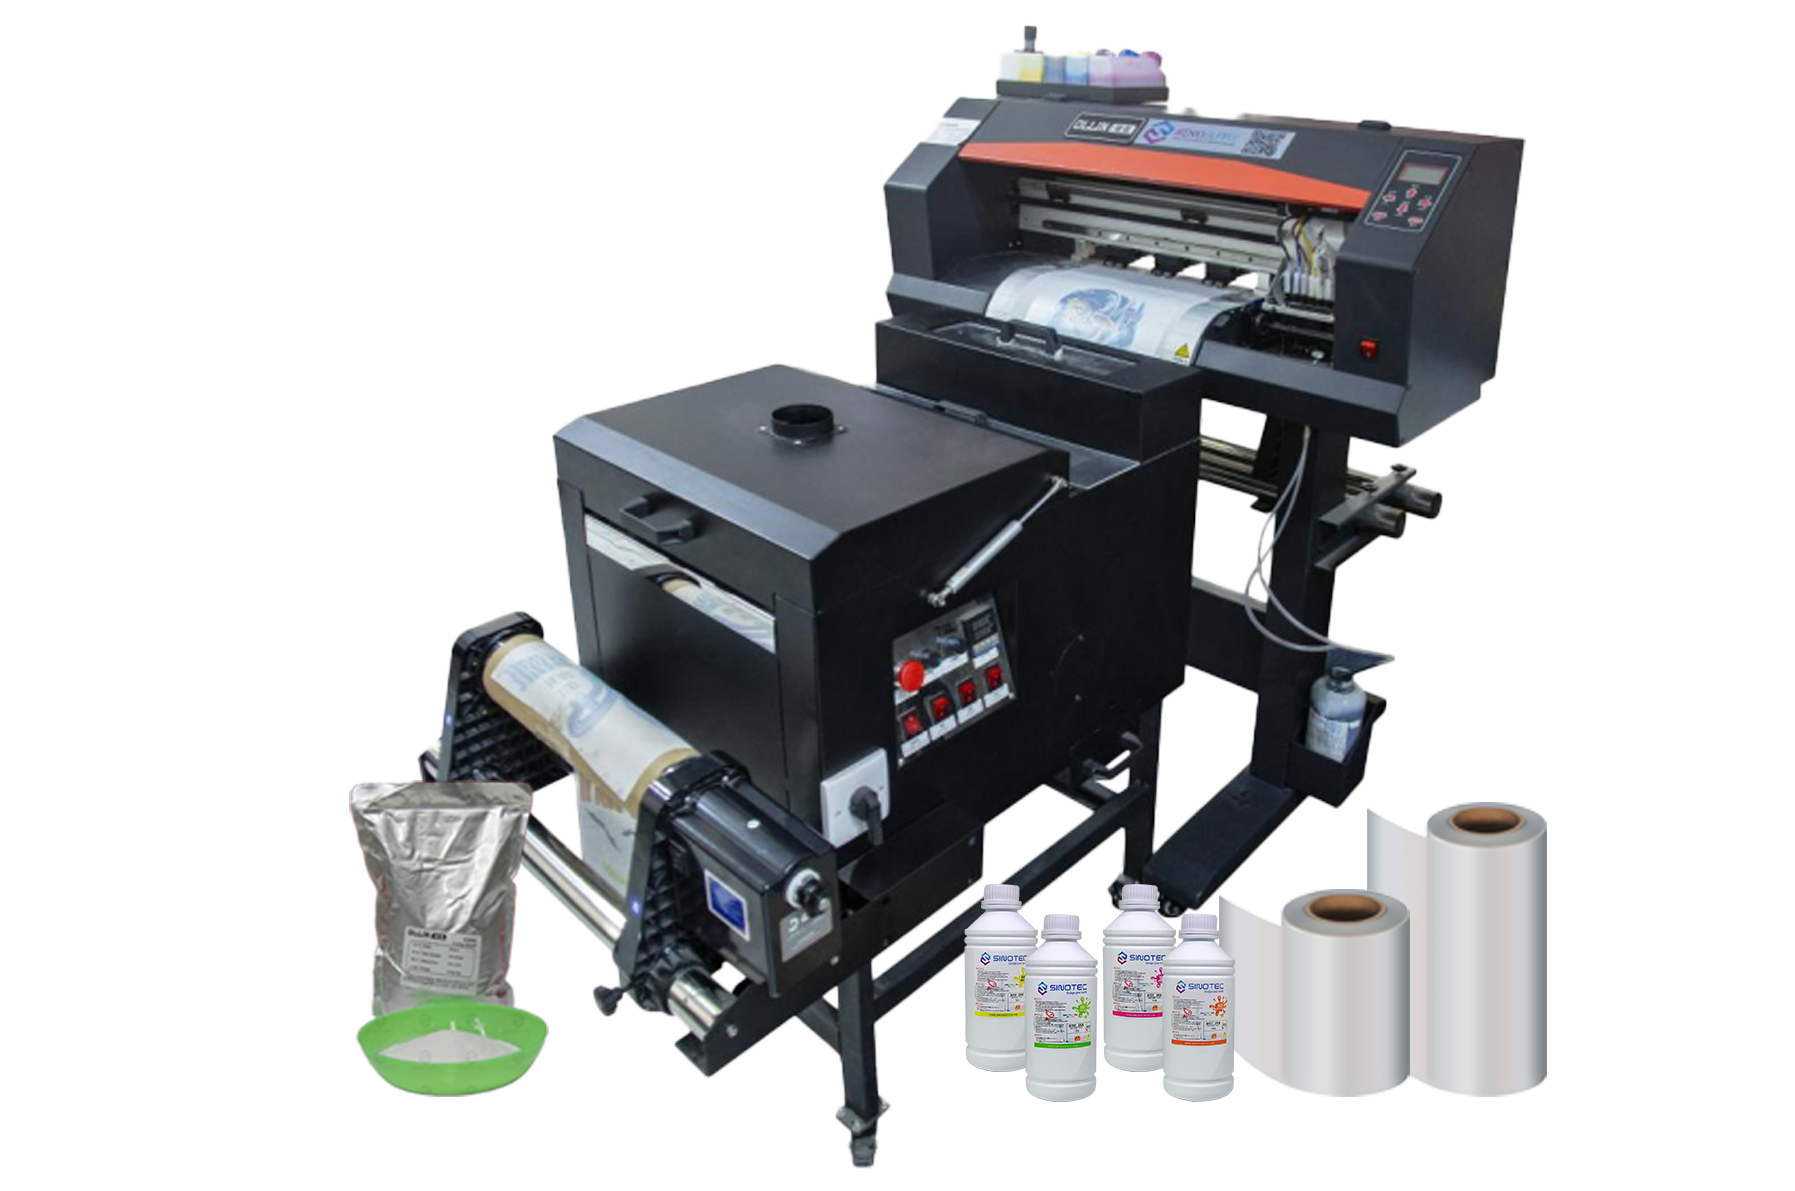
DTF printing machine

Small DTF Printer vs. Full-Scale Setup: Matching Equipment Scale to Production Volume and Budget

Scale mismatch is one of the more avoidable procurement errors in DTF printing — and yet it happens consistently. Buyers either over-specify for a production volume that doesn’t justify the capital outlay, or they under-buy and find themselves bottlenecked within the first quarter of operation. Neither outcome is acceptable when the equipment decision anchors a broader fulfillment workflow.

A small DTF printer — typically a single-head unit with a narrower print bed — suits operations running limited daily volumes, short-run custom orders, or sampling workflows where flexibility matters more than throughput. The entry point for these units is substantially lower, both in acquisition cost and in facility requirements. A desktop DTF printer takes this further: compact enough for constrained production spaces, it removes the ventilation, power, and floor-space overhead that larger roll-fed systems demand. For procurement managers sourcing equipment for regional decorators, startup fulfillment centers, or pilot programs, these formats offer a lower-risk entry into DTF production without committing to industrial-grade infrastructure.

Full-scale setups tell a different story. Multi-head configurations, wider print widths, and integrated powder-shaking and curing systems are built for sustained daily output — the kind of volume where per-unit economics only work if the machine runs near capacity. The capital cost is higher, the lead time on sourcing and installation is longer, and the staffing requirements shift meaningfully. These aren’t drawbacks — they’re simply the operating realities of production-grade DTF printing machine investment.

Equipment TierTypical Use CaseKey Procurement Consideration
Desktop / Small FormatSampling, short-run, pilot programsLow overhead; evaluate upgrade path before committing
Mid-Range Single-HeadSmall-batch commercial productionBalance between throughput and operational cost
Multi-Head / Wide FormatHigh-volume fulfillment operationsFacility readiness and staffing must be pre-qualified

The practical question isn’t which tier is better — it’s which tier matches current volume with realistic growth headroom. Suppliers who offer modular configurations or phased upgrade paths give buyers considerably more room to scale without forcing a full equipment replacement cycle prematurely.

Desktop DTF Printer Procurement Criteria: Supplier Specs, Certifications, and What to Verify Before You Commit

Procurement decisions for a desktop DTF printer carry more risk than their compact footprint suggests. The unit cost may be lower than industrial-grade equipment, but the supplier relationship — and what it delivers in terms of documentation, suporte pós-venda, and specification transparency — determines whether that machine earns its place in a production workflow or becomes an expensive liability within six months.

Start with certifications. Any DTF printing machine entering a regulated export market should carry CE marking for European distribution and FCC compliance for North American buyers at minimum. RoHS compliance matters too, particularly for buyers operating under corporate sustainability requirements or supplying retail chains with environmental sourcing policies. Suppliers who cannot produce current, verifiable certificates — not just logos on a product page — should be disqualified early in the evaluation process.

Specification verification is where most procurement errors happen. A supplier’s published spec sheet and the actual unit performance frequently diverge on print resolution, ink consumption rates, and duty cycle limits. Before committing, request third-party test reports or, where volume justifies it, arrange a factory sample run using your own artwork files. A small DTF printer marketed for commercial sampling should demonstrate consistent adhesion results across fabric types — not just on optimized demo substrates. If a supplier resists this, that tells you something.

The procurement checklist for this category should cover:

  • OEM/ODM capability — can the supplier adjust printhead configuration, ink system, or firmware to match your operational requirements
  • MOQ flexibility — especially relevant for buyers piloting a desktop DTF printer before scaling to higher-throughput configurations
  • Lead time commitments documented in writing, not quoted verbally during sales calls
  • Spare parts availability and documented service intervals for printheads and curing components
  • Export compliance support — HS code documentation, packing standards, and freight coordination capacity

Suppliers with established export infrastructure — the kind that handles customs documentation, manages QC at the production stage, and maintains responsive project coordination — reduce the operational burden on the buyer’s side considerably. That’s not a minor convenience. For cross-border procurement, it’s a structural advantage that compounds over the life of the supplier relationship.
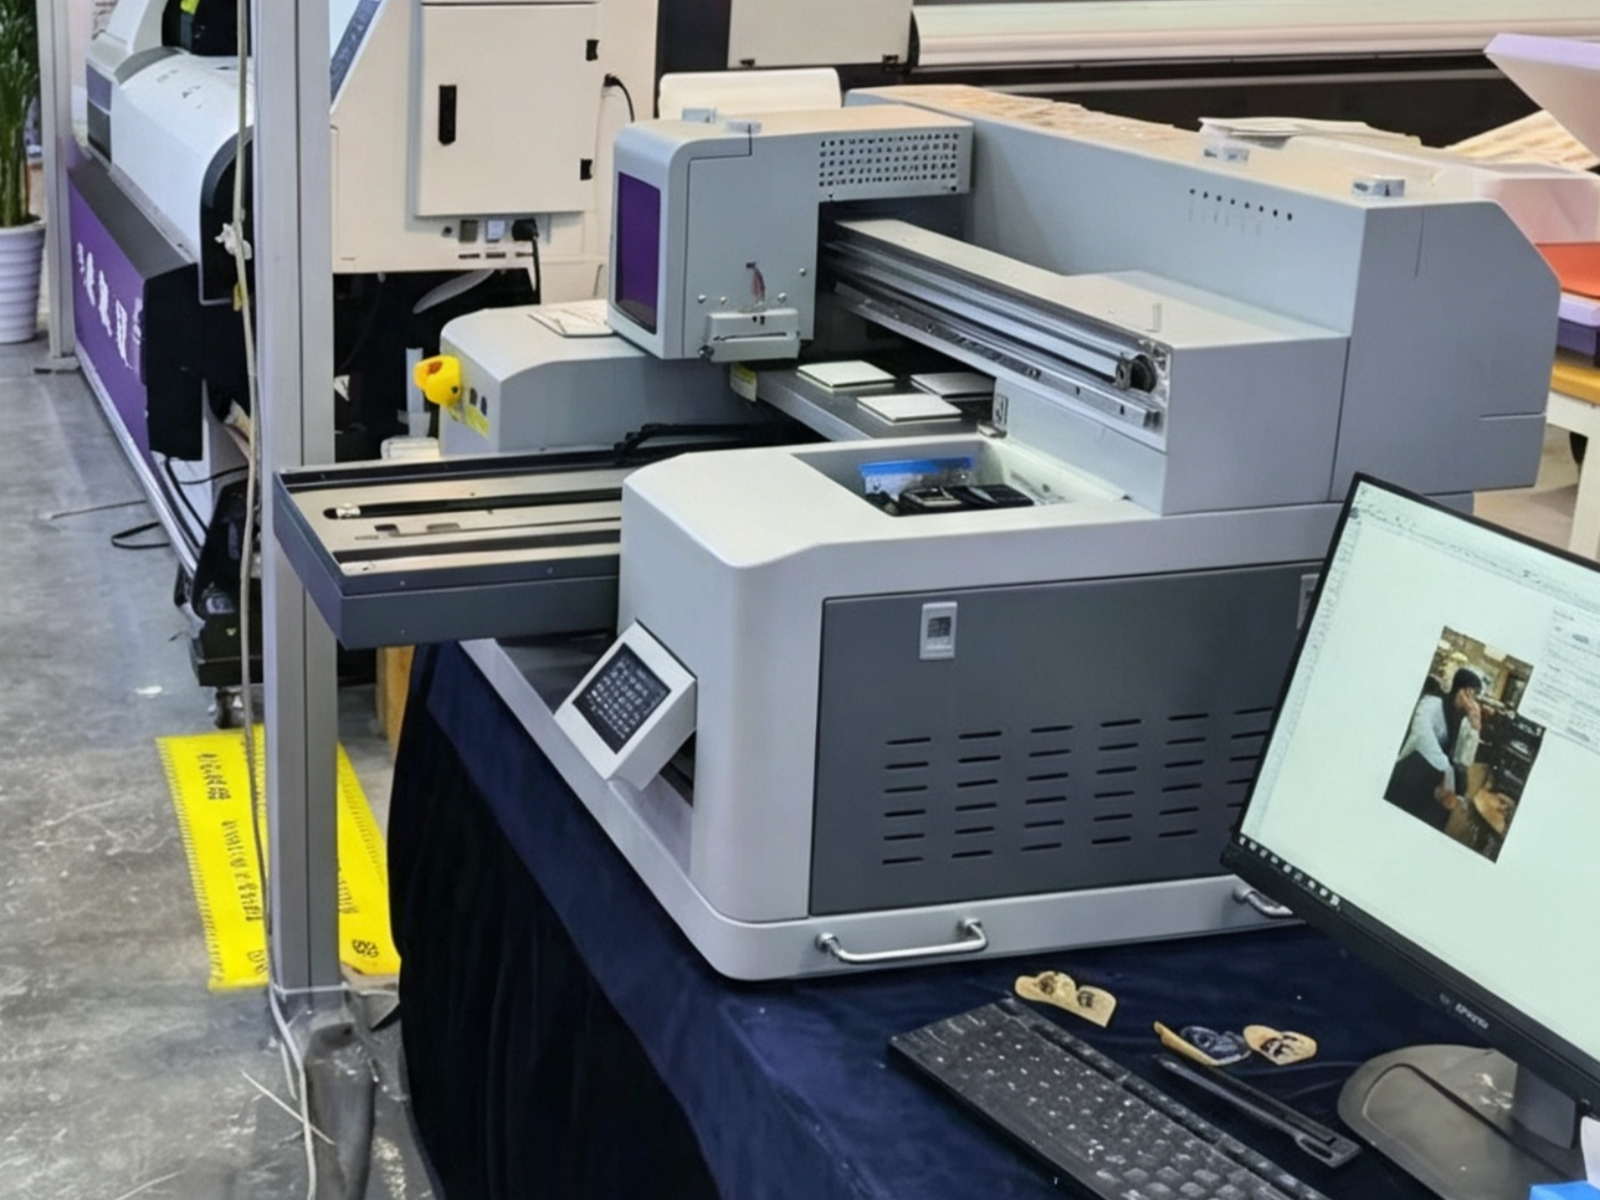
Máquina de impressão DTF

Shaker, Curing Unit, Heat Press, and Ventilation: How to Source the Full DTF Workflow Stack Without Gaps

The DTF printing machine gets most of the attention in procurement conversations — but the workflow gaps that actually stall production almost always sit in the peripheral equipment. A shaker, a curing unit, a heat press, and a properly ventilated workspace aren’t optional add-ons. They’re load-bearing components of a functional DTF operation, and sourcing them as an afterthought creates real operational risk.

Start with the powder shaker and curing unit. These two are often bundled with mid-range and high-volume DTF systems, but buyers scaling from a desktop DTF printer configuration frequently discover that the bundled unit doesn’t match their actual throughput. The shaker needs to distribute adhesive powder evenly across the printed film — inconsistent coverage at this stage causes adhesion failures downstream, regardless of print quality. Curing unit specs, particularly temperature uniformity and belt speed, must align with the ink and film combinations the printer uses. Mismatches here don’t show up as obvious defects; they show up as garments failing after the first wash cycle.

Heat press sourcing deserves its own evaluation process. Pressure consistency, platen size relative to the print format, and temperature accuracy across the full platen surface are the criteria that matter. A small DTF printer running A4-width film doesn’t require the same press spec as a 60cm roll-fed system — but both need a press that holds calibration under continuous commercial use, not just in a demo setting.

  • Confirm that shaker belt dimensions match the film width your DTF printing machine outputs
  • Request curing unit temperature uniformity data, not just rated temperature ranges
  • Verify heat press platen size against your maximum print dimensions with margin
  • Specify ventilation requirements to your facility manager before equipment arrives — fume extraction is a compliance issue in most commercial environments, not a preference
  • Confirm that peripheral equipment lead times are coordinated with the main unit delivery, not treated as separate procurement tracks

Suppliers with integrated product lines — where the DTF printing machine, shaker, and curing components are designed and tested together — reduce compatibility risk considerably. For cross-border buyers, coordinating this full stack through a single supplier with export documentation capability also simplifies freight logistics and customs classification across multiple equipment categories.

Conclusão

The equipment itself is only half the decision — the peripheral stack around it determines whether your setup actually runs at production capacity or spends half its time compensating for compatibility gaps.

If there’s one thing worth repeating: don’t treat a DTF printing machine as a standalone purchase. Spec the shaker, curing unit, and heat press together, confirm temperature uniformity before you commit, and — especially for international buyers — coordinate lead times so nothing sits idle waiting on a component that got routed through a separate freight channel.

Get the full stack right from the start, and the production math takes care of itself.

Frequently Asked Questions

P: What is a DTF printing machine and how does it work?

UM: A DTF printing machine prints designs onto a special PET film using water-based inks, then a hot-melt adhesive powder is applied and cured — the finished transfer is then pressed onto fabric using a heat press. Unlike screen printing, there are no screens to burn and no minimum run requirements, which makes it practical for short runs and custom orders without the setup overhead.

P: What materials can a DTF printing machine print on?

UM: DTF transfers bond to a wide range of fabrics — cotton, poliéster, nylon, jeans, couro, and blends — without requiring the garment to be pre-treated. That versatility is one of the main reasons DTF has displaced DTG for buyers who work across multiple fabric types rather than cotton-only runs.

P: How much does a DTF printing machine cost?

UM: Entry-level desktop units typically start in the low thousands, while production-grade wide-format DTF printing machines can run considerably higher — and that’s before you factor in the shaker, curing unit, and heat press that the full workflow actually requires. Budget for the complete peripheral stack upfront rather than discovering the gaps after delivery.

P: Why does a DTF printing machine need a powder shaker and curing oven?

UM: The hot-melt adhesive powder won’t bond evenly to the film — or cure at the right melt point — without controlled agitation and heat. Skipping a dedicated shaker and curing unit and trying to improvise those steps is one of the fastest ways to end up with transfers that peel or crack after the first wash.

P: How long do DTF transfers last on fabric?

UM: A properly cured DTF transfer — pressed at the correct temperature and pressure — typically holds up through dozens of wash cycles without significant cracking or fading. Durability drops noticeably when the curing step is rushed or the heat press temperature is inconsistent, so temperature uniformity across the platen matters more than most buyers expect.

P: Can a DTF printing machine replace a screen printing setup?

UM: For short runs, multi-color designs, and on-demand fulfillment, a DTF printing machine is genuinely more efficient than screen printing — no film positives, no emulsion, no per-color setup cost. Screen printing still wins on unit economics at very high volumes for simple designs, so the honest answer depends entirely on your order profile.

P: Is a DTF printing machine worth it for small businesses?

UM: For operations doing custom apparel, promotional merchandise, or print-on-demand — even at modest volumes — the economics tend to work in DTF’s favor faster than most people expect. The real calculation isn’t just the machine cost; it’s whether your order volume justifies owning the full production stack versus outsourcing transfers from a trade supplier.

P: How do I choose the right print width for a DTF printing machine?

UM: Print width should match your most common substrate size — a 30cm unit handles standard garment graphics, while wider formats (60cm and above) open up all-over prints, cut-and-sew panels, and soft signage without tiling. Buyers sourcing through OEM channels — suppliers like SINOTEC who handle customized specifications — can often configure print width and ink channel layout to match a specific production use case rather than defaulting to a catalog spec.
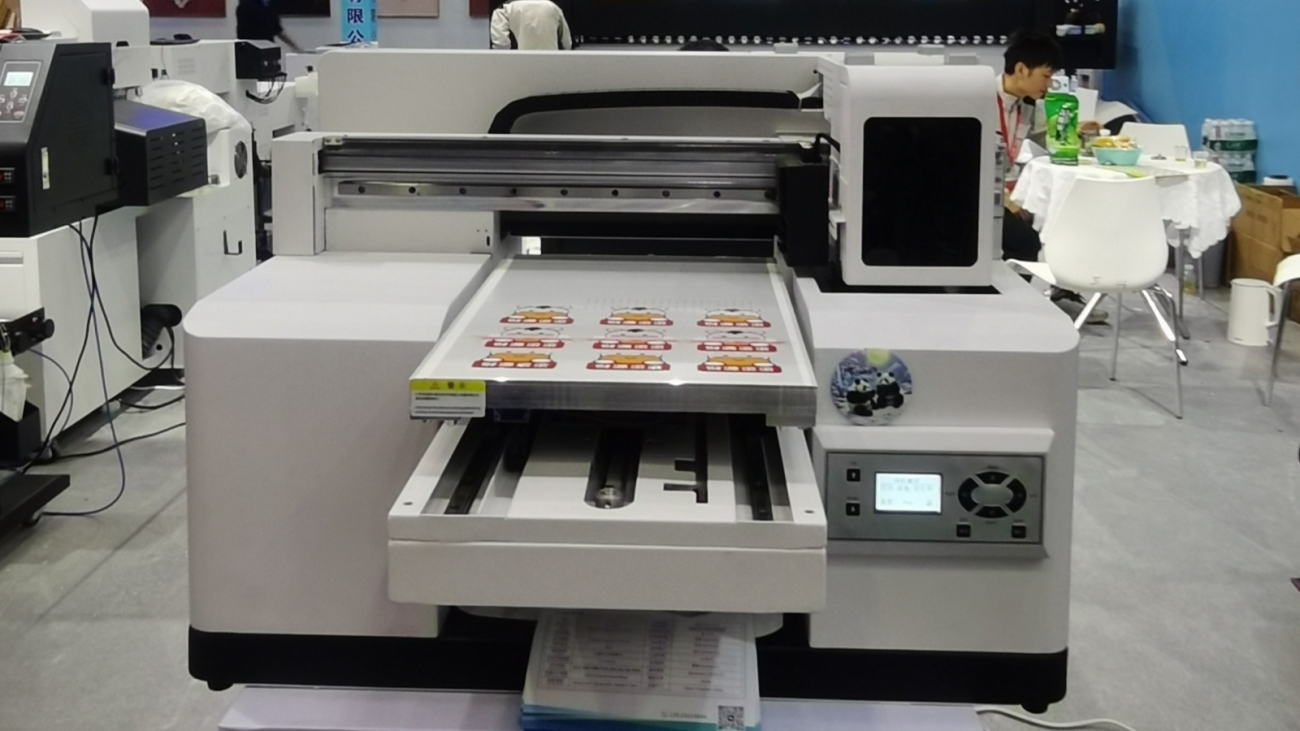
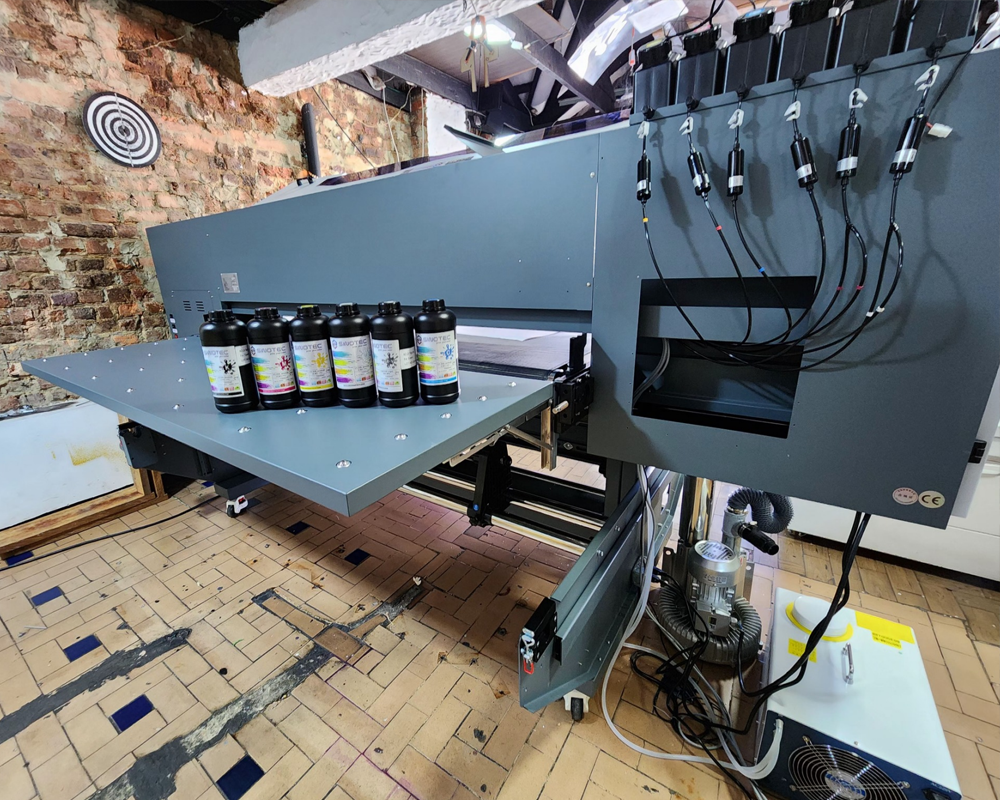
Impressora UV

Fornecimento de impressora UV: Como qualificar o fornecedor certo

Qualifying a Impressora UV supplier is not a single conversation — it’s a structured evaluation that separates vendors who can fulfill a one-time order from partners who can support long-term production demands. The stakes are higher than most buyers expect, particularly when the end application involves specialized substrates, tight color tolerances, or regulated industries where output consistency is non-negotiable.

Start with capability verification, not pricing. A supplier quoting aggressively on a commercial UV printer configuration means very little if they cannot demonstrate ink adhesion performance across the substrate range your operation actually uses. Request sample outputs on your specific materials — rigid boards, textured surfaces, curved panels — before any commercial discussion moves forward. Suppliers with genuine production depth will accommodate this without hesitation.

Certifications matter more at the industrial end of the market. When sourcing an industrial UV printer for high-volume or export-facing production, relevant compliance documentation — CE marking, RoHS conformity, or regional electrical safety standards — directly affects your ability to deploy equipment across different markets without regulatory friction. Ask for documentation upfront, not as an afterthought during contract review.

There are four operational criteria worth pressing on during supplier qualification:

  • Lead time transparency — confirmed production and shipping timelines, not estimated ranges that shift after deposit
  • OEM/ODM flexibility — whether the supplier can accommodate custom configurations, ink system modifications, or branded hardware specifications
  • After-sales infrastructure — availability of spare parts, firmware support, and technical response time for equipment faults
  • MOQ and order scalability — minimum order thresholds and whether pricing structures hold as volume increases

Suppliers like SINOTEC — operating out of China with an export-oriented fulfillment model — illustrate what responsive project coordination can look like at the sourcing stage: customized specifications managed before production, not corrected after delivery. That kind of upstream involvement reduces costly rework cycles and keeps procurement timelines intact.

One detail buyers routinely underweight: quality control protocols at the factory level. A supplier’s internal inspection process — print resolution checks, UV lamp output verification, substrate feed calibration — is a direct proxy for the consistency you’ll receive across repeat orders. Ask how defects are caught, not just how they’re handled after the fact.

What Actually Separates a Reliable UV Printer Supplier from a Risky One

Supplier reliability in the UV printer category isn’t something you can assess from a product listing alone. The gaps — the ones that cause missed deadlines, inconsistent output, or warranty disputes — almost always trace back to operational factors that never appear on a spec sheet.

Start with production transparency. A credible supplier should be able to walk you through their manufacturing process for a commercial UV printer: how print heads are sourced and tested, what substrate compatibility validation looks like, and whether QC checkpoints exist mid-production or only at final inspection. Suppliers who can only speak to the end result — not the process — are a procurement risk.

Certifications matter, but context matters more. CE, RoHS, and FCC markings confirm baseline compliance for target export markets. What they don’t confirm is whether a given supplier’s industrial UV printer line has been validated for the specific substrates, ink formulations, or duty cycles your operation requires. Push for documentation that’s specific to your use case, not just general compliance certificates attached to a product category.

  • Request production audit reports or third-party inspection records — not just supplier-authored datasheets
  • Confirm whether OEM/ODM customization is handled in-house or subcontracted, as subcontracting adds opacity to quality control
  • Clarify lead times for both standard and custom configurations — and whether those timelines hold during peak export periods
  • Ask specifically how the supplier handles specification deviations discovered post-production

Responsiveness during the pre-order phase is a reliable signal. Suppliers who engage seriously with technical questions before a purchase order is placed — adjusting specifications, flagging compatibility issues, coordinating on packaging or export documentation — tend to carry that same rigor into production. Suppliers who only become communicative after payment rarely improve from there.

The distinction between a manageable supplier relationship and a costly one often comes down to upstream involvement. Buyers sourcing through export-oriented suppliers — particularly those offering structured OEM support — benefit most when that coordination begins at the specification stage, not after the first shipment arrives with problems that were entirely avoidable.

Impressora UV

How to Evaluate Commercial UV Printer Specs Against Your Real Production Needs

Spec sheets for a commercial UV printer are designed to impress — and they usually succeed, at least on paper. The practical question for procurement managers is whether those specifications map to what production actually demands, week over week, at volume. That gap between headline specs and operational reality is where most sourcing decisions go wrong.

Print resolution is the obvious starting point, but it’s rarely the limiting factor. A UV printer rated at 1440 dpi is meaningless if the substrate handling system can’t maintain registration on rigid materials, or if the curing lamp intensity degrades faster than the manufacturer’s warranty implies. Buyers sourcing for high-throughput applications — signage, packaging prototypes, industrial components — should weight throughput speed and duty cycle far more heavily than peak resolution figures.

A few evaluation criteria tend to separate genuinely capable machines from those that look strong on a datasheet:

  • Printable area versus usable print area — some machines lose significant working space at the edges due to carriage mechanics
  • Ink system compatibility — whether the machine is locked to proprietary inks, and what that means for long-term consumable costs
  • Curing system type and lamp lifespan — UV LED systems run cooler and last longer than mercury-arc alternatives, which matters for heat-sensitive substrates
  • Maximum substrate thickness and weight — often understated in marketing materials but critical for industrial UV printer applications involving rigid or layered materials
  • Software integration — RIP software compatibility, file format support, and whether color profiles are included or sold separately

Duty cycle deserves particular attention. A machine rated for intermittent commercial use will degrade noticeably under continuous production schedules — and the cost of unplanned downtime in a production environment compounds fast. Buyers should request documentation on mean time between failures and ask suppliers directly how the machine performs under sustained load, not just during demonstration runs.

Suppliers with structured OEM and specification support — the kind that can adjust configurations to match a buyer’s substrate range or ink requirements before production — tend to surface these trade-offs early. That upstream technical engagement is worth factoring into supplier selection, not just the per-unit price.

Impressora UV

Industrial UV Printer Certifications, MOQs, and Lead Times: What to Demand Before You Commit

Certifications are not paperwork formalities — they are operational risk controls. For any Industrial UV Printer destined for a regulated production environment, the relevant compliance marks (CE for European markets, FCC for North American electrical standards, RoHS for hazardous substance restrictions) tell a buyer whether the machine can legally operate in their facility and whether the ink chemistry meets environmental obligations. Asking a supplier for certification documentation before signing a purchase order is standard practice; accepting verbal assurances in place of actual certificates is not.

Beyond compliance, UV printer certifications also signal something about the manufacturer’s internal quality discipline. A supplier who has maintained ISO 9001 certification across multiple audit cycles has demonstrated process consistency — which matters when you are ordering at volume and cannot inspect every unit before it ships.

MOQ structures vary considerably across the supplier landscape. Some manufacturers set minimum order quantities at a single unit for commercial-grade models, particularly where the machine price already reflects a significant capital commitment. Others — especially those offering OEM or customized specification builds — require minimum runs of three to five units before they will absorb tooling or configuration costs. Buyers sourcing a Commercial UV Printer for a multi-site rollout should negotiate MOQ terms early, since the threshold directly affects cash flow planning and phased deployment schedules.

  • Request written certification copies, not just model numbers listed on a spec sheet
  • Confirm whether certifications apply to the specific configuration being ordered, not just the base model
  • Clarify whether MOQ applies per SKU or across a combined order
  • Get lead time commitments in writing — standard production runs versus peak-season delays are rarely the same figure

Lead times deserve the same scrutiny. A UV printer supplier quoting four to six weeks under normal conditions may quietly extend that window during high-demand periods without proactive communication. Procurement managers should establish contractual lead time benchmarks with defined escalation clauses — and ask specifically whether the quoted timeline covers production only, or includes pre-shipment quality inspection and export documentation. Suppliers with established export workflows and dedicated project coordination tend to absorb those logistics variables more reliably than those handling international orders on an ad hoc basis.

Conclusão

The right UV printer purchase comes down to two things: honest spec verification and a supplier who treats lead times as a commitment, not an estimate.

So much of the frustration buyers run into — mismatched configurations, blown timelines, certification gaps — traces back to questions that weren’t asked early enough. Get those answers in writing before the order is placed, not after the deposit clears. Suppliers with real export infrastructure and dedicated project coordination will answer those questions without hesitation. The ones who hedge or deflect? That’s your answer too.

Do your homework upfront, and the hardware almost takes care of itself.

Frequently Asked Questions

P: What is a UV printer and how does it work?

UM: A UV printer uses ultraviolet light to instantly cure — or harden — ink as it’s deposited onto a surface, rather than letting it air-dry or absorb into the material. That curing process is what makes UV printing so versatile: the ink bonds to almost any substrate, rigid or flexible, without soaking in. The result is sharp, durable output that traditional inkjet simply can’t replicate on non-porous materials.

P: What materials can a UV printer print on?

UM: The substrate range is genuinely broad — wood, vidro, metal, acrílico, couro, ceramic tile, phone cases, and most rigid plastics are all fair game. Some UV printers also handle flexible materials like TPU or certain fabrics when paired with the right ink formulation. The main limitation is surface flatness and the machine’s Z-axis clearance (the maximum object height it can accommodate).

P: How much does a UV printer cost?

UM: Entry-level desktop UV printers typically start in the low thousands, while mid-range flatbed units for commercial use often land somewhere between mid-five and low-six figures depending on print area and ink channel configuration. Industrial-grade wide-format UV printers can go considerably higher. The hardware price is only part of the equation — ink costs, maintenance contracts, and replacement lamp or LED components add up over the machine’s lifespan.

P: Is a UV printer worth it for small businesses?

UM: It depends almost entirely on order volume and product mix. A UV printer earns its keep quickly when you’re producing customized promotional items, sinalização, or personalized products at consistent volume — the per-unit cost drops fast once setup costs are absorbed. For very low-volume or highly irregular work, outsourcing UV print jobs often makes more financial sense than owning the equipment outright.

P: How long do UV printer prints last?

UM: UV-cured prints are generally more resistant to fading, moisture, and abrasion than solvent or dye-based alternatives — outdoor-rated UV inks on properly prepared substrates can hold up for several years under direct exposure. Indoor applications with no UV stress typically last much longer. Longevity is also affected by surface prep, ink quality, and whether a protective varnish layer was applied during printing.

P: Can a UV printer print white ink?

UM: Most commercial UV printers include a dedicated white ink channel — this is essential for printing on dark, transparent, or metallic surfaces where CMYK alone would be invisible or washed out. White ink does require more maintenance than color channels; it tends to settle and clog faster, so machines need regular circulation or purging cycles to keep it printing cleanly. Buyers sourcing through OEM or wholesale channels should confirm white ink channel support before finalizing specs.

P: Why is my UV printer leaving streaks or missing lines?

UM: Streaking and banding almost always trace back to one of three culprits: clogged or partially blocked printheads, incorrect media height settings, or UV lamp output that’s degraded below effective curing intensity. Running a nozzle check and printhead cleaning cycle is the first step — if that doesn’t resolve it, check lamp hours against the manufacturer’s replacement threshold. Consistent environmental conditions (temperature and humidity) matter more than most buyers realize when it comes to UV ink behavior.

P: How do I choose the right UV printer for my application?

UM: Start with your substrate requirements and maximum object dimensions, then work backward to print area, Z-axis clearance, and ink configuration. Resolution specs matter, but they’re often overstated in marketing — real-world output quality depends as much on ink chemistry and printhead type as on the DPI figure. Suppliers with genuine OEM and customization capability, like those coordinating export-oriented orders for international buyers, can often adjust configurations to match specific production requirements rather than forcing a standard SKU.

SEO Metadata Reference

SEO Title: Fornecimento de impressora UV: Como qualificar o fornecedor certo

Meta Description: Learn UV printer supplier qualification the right way — verify capabilities, check certifications, and avoid costly sourcing mistakes before signing anything.

eco solvent printing machine

Especificações da máquina de impressão com solvente ecológico que realmente movem a agulha no ROI

Specs on paper are cheap. Every supplier has a datasheet that looks impressive until you actually try to map it against a real production environment and realize half the numbers are best-case-scenario figures measured under lab conditions nobody operates in.

So here’s what actually matters when you’re evaluating an eco solvent printing machine for commercial ROI — and it’s not the headline resolution figure everyone leads with.

Print speed-to-quality ratio is the first real lever. A machine rated at 60 sqm/hr in “production mode” might drop to 28 sqm/hr the moment you push it to a quality tier your clients actually accept. That gap — between rated speed and usable speed — is where margins quietly disappear. Ask suppliers for output figures at draft, production, and high-quality modes separately. If they can only give you one number, that’s a red flag worth noting.

Ink consumption per square meter is the other number that procurement teams consistently underweight at the sourcing stage. Eco-solvent ink isn’t the cheapest consumable in your supply chain, and on a large eco solvent printer running banner and fleet graphics work at volume, um 15% difference in ink draw between two machines translates to a surprisingly significant annual cost delta — easily $8,000–$12,000 over a three-year run depending on throughput.

Then there’s media compatibility. Wider carriage width (1.6m vs. 1.8m vs. 2.5m+) isn’t just a size spec — it determines which substrate categories you can serve. An eco solvent digital printer that handles vinyl, tela, backlit film, and floor graphics without constant head-height recalibration keeps your setup time low and your operator frustration lower.

Spec CategoryWhat Buyers Usually CheckWhat Actually Drives ROI
Print SpeedMax rated sqm/hrUsable speed at production-quality mode
Ink SystemNumber of colorsInk consumption per sqm at working mode
Media WidthMax roll widthSubstrate range without manual reconfiguration
ManutençãoWarranty periodHead cleaning cycle frequency and ink waste volume

And the maintenance angle is genuinely underrated (most buyers don’t ask about it until they’re already losing hours to it). Printhead cleaning cycles that waste 3–5ml of ink per purge, multiplied across daily operations, add up fast. Suppliers who can provide documented maintenance schedules with real consumable cost breakdowns — not just warranty language — are the ones worth having a longer conversation with.

eco solvent printing machine

Which Eco Solvent Digital Printer Specs Translate Directly to Lower Cost-Per-Print

Spec sheets lie. Not deliberately — but a printer rated at 50 sqm/hr in “production mode” and one rated at 32 sqm/hr in “quality mode” aren’t actually that far apart once you’re running real jobs on real substrates. The number that matters isn’t peak throughput. It’s throughput at the resolution your clients actually need.

So here’s where procurement managers tend to leave money on the table: they optimize for purchase price and ignore the specs that drive ongoing cost-per-print. A large eco solvent printer with a lower sticker price but a 4-pass minimum for acceptable outdoor quality will cost you more per square meter over 18 months than a mid-range unit hitting the same output in 2 passes. The math is unflattering and it compounds fast.

The specs that actually move the needle on cost-per-print:

  • Ink drop size (picoliters) — smaller drops (3–7pl variable) mean less ink wasted on coverage you don’t need
  • Pass count at working resolution — fewer passes at your target DPI = more output per shift
  • Printhead channel count — more channels per head reduces redundant passes on wide-format jobs
  • Ink consumption rate at production mode — documented ml/sqm figures, not marketing estimates
  • Drying and curing speed — a slow cure system bottlenecks your finishing line regardless of print speed

The drying spec is one buyers consistently underweight (especially on roll-to-roll setups where media piles up if the heater can’t keep pace). An eco solvent digital printer running at 35 sqm/hr with an underpowered heating array is effectively running slower than that — because your operator is waiting on the output end.

And ink system architecture matters more than color count alone. An 8-color system with poor channel isolation will still waste ink on every purge cycle. Suppliers who publish actual ml-per-purge figures — not just “low ink waste” in the brochure — are telling you something real about how the machine was engineered. SINOTEC, for example, provides documented consumable specs as part of its OEM configuration process, which makes this comparison actually possible before you commit.

Bottom line: match the spec to the job type. Not the other way around.

Large Eco Solvent Printer Configurations: Matching Print Width and Throughput to Commercial Volume

Print width is one of those specs that looks simple on paper and turns into a real operational headache if you get it wrong at the procurement stage. A large eco solvent printer running a 3.2-meter carriage might sound like future-proofing — and sometimes it is — but if your average job is 1.6-meter banner stock, you’re heating a platen twice the size you need on every single run. That’s not a minor inefficiency. That compounds.

So here’s how to think about this practically. Commercial volume breaks into three rough tiers: high-mix/low-volume shops (sinalização, event graphics, short runs), mid-volume production environments (fleet graphics, retail POS, recurring contracts), and dedicated high-throughput facilities running continuous shifts. Each tier has a different answer for optimal print width — and honestly, optimal throughput spec too.

Operation TypeRecommended Print WidthTarget ThroughputKey Configuration Priority
High-mix / short run1.6m – 1.8m20–35 sqm/hrMedia flexibility, fast job switching
Mid-volume production1.8m – 2.5m35–60 sqm/hrConsistent output quality, ink economy
High-throughput / continuous2.5m – 3.2m60–100+ sqm/hrDual-head arrays, automated media handling

And this is where buyer conversations with suppliers often go sideways. Procurement teams ask for the highest throughput number available — understandable — without asking what configuration produces that number. Peak throughput figures on an eco solvent digital printer spec sheet are almost always measured in draft or production mode, not in the print quality setting your actual clients will expect. Big difference. Worth asking explicitly.

Configuration matters beyond just the carriage. Dual-CMYK head layouts, tandem printing modes, and automated take-up systems are what separate a machine rated at 80 sqm/hr that actually delivers 80 sqm/hr from one that tops out at 55 under real conditions. Suppliers like SINOTEC who support OEM configuration give buyers the ability to spec these elements upfront — not retrofit them later at cost.

Fit the machine to the volume you have now, with a ceiling for where you’ll realistically be in two years. Not the theoretical maximum. That’s the procurement call that actually pays off.

eco solvent printing machine

Supplier Evaluation Criteria for Eco Solvent Printing Machines: Certifications, Lead Times, and OEM Flexibility

Certifications are not a formality. For procurement managers sourcing an eco solvent printing machine across borders, they’re the first real filter — and a lot of suppliers know how to look compliant without actually being compliant.

So here’s what to actually check. CE marking matters for European import. RoHS compliance tells you the electronics aren’t going to create a disposal headache three years from now. ISO 9001 certification on the manufacturing process — not just claimed, but audited — is the baseline for any serious volume order. And if you’re buying a large eco solvent printer destined for a North American market, confirm UL or ETL electrical certification before the unit ships, not after it clears customs (that mistake costs more than the freight).

Lead times are where a lot of sourcing decisions quietly fall apart. Standard production lead times from Chinese manufacturers on an eco solvent digital printer typically run 15 to 35 working days depending on configuration complexity and order volume. But that number assumes your specs are locked, your deposit is cleared, and there’s no CNY window or peak export season involved. Ask for a production schedule in writing. Ask what happens if a printhead is backordered — Epson i3200 heads, for instance, have had supply constraints that rippled into delivery delays across the industry.

OEM flexibility is where suppliers actually separate themselves. Not every manufacturer will touch custom firmware, rebadged control panels, or spec-built ink delivery systems. Suppliers like SINOTEC operate specifically within OEM and ODM frameworks, which means buyers can negotiate configurations upfront rather than inheriting a standard build and working around its limitations.

  • Minimum order quantities for OEM runs — know the threshold before you negotiate
  • Sample unit availability before full production commitment
  • Documentation support: CE declarations, test reports, user manuals in your market language
  • After-sales terms: parts warranty period, remote tech support, and local service partner availability

Rigid. That’s what a supplier with no OEM flexibility is. And that rigidity compounds every time your client brief changes.

Conclusão

Buying an eco solvent printing machine isn’t complicated — but buying the right one absolutely is. Ink compatibility, manipulação de mídia, and supplier flexibility aren’t checkbox items; they’re the difference between a machine that earns its place on your floor and one that quietly drains your margins through workarounds and downtime.

OEM flexibility matters more than most buyers realize until it’s too late.

So before you commit: push your supplier on configurations, ask for a sample unit, and get the after-sales terms in writing. The specs on a datasheet are just the starting point — what happens after the invoice is where the real story begins.

Frequently Asked Questions

P: What is an eco solvent printing machine and how is it different from a regular solvent printer?

UM: An eco solvent printing machine uses a milder, petroleum-derived ink that produces far fewer volatile organic compounds than traditional harsh-solvent printers — so you can run it in a standard workspace without industrial ventilation. The trade-off is that eco solvent inks are slightly less aggressive on media adhesion, but for most commercial signage and vehicle wrap applications, the difference is negligible.

P: How long does eco solvent ink actually last on outdoor prints?

UM: Unlaminated, you’re realistically looking at 2–3 years of outdoor durability before fading becomes noticeable. Add a UV-protective laminate and that figure jumps to 5+ years — which is why most professional print shops laminate anything going on a vehicle or storefront.

P: How much does an eco solvent printing machine cost?

UM: Entry-level desktop units start around $3,000–$5,000, but a production-grade wide-format eco solvent printer — something from Roland, Mimaki, or a configurable OEM unit — will run anywhere from $12,000 to $40,000 depending on print width, speed, and ink configuration. Don’t anchor on sticker price alone; ink cost per liter and head replacement intervals are where the real margin math happens.

P: Can I use third-party inks in an eco solvent printing machine?

UM: Technically yes, practically — it depends on the machine’s firmware and whether your supplier locks the ink system. Some OEM-configured units, particularly those sourced through suppliers like SINOTEC that offer open ink system options, give you that flexibility from the start. Going third-party on a locked system risks voiding your warranty and, worse, clogging printheads that cost $800–$2,000 to replace.

P: Why does my eco solvent printer keep clogging printheads?

UM: Nine times out of ten it’s one of three things: the machine sat idle for too long without a maintenance flush, the ambient temperature dropped below the ink’s operating range (most eco solvent inks want 64–86°F), or there’s an ink compatibility issue. Run a nozzle check every morning before printing — it takes 90 seconds and saves you from a $1,500 head replacement.

P: Is an eco solvent printing machine worth it for a small print shop?

UM: For a shop doing vehicle wraps, bandeiras, or retail POS graphics — absolutely. The output quality is strong enough for high-margin work, and you’re not dealing with the safety overhead of aggressive solvent systems. Where it gets dicey is if your volume is genuinely low; a machine sitting idle eats ink through maintenance cycles and the ROI math gets ugly fast.

P: What media can an eco solvent printing machine print on?

UM: The range is broad — vinyl (cast and calendered), banner material, tela, coated paper, window film, and most transfer substrates. What it won’t handle is uncoated textiles or rigid boards thicker than roughly 1mm, since eco solvent is a roll-fed format. If you’re regularly printing on rigid substrates, you’d need a UV flatbed in your lineup.

P: How do I choose between a 64-inch and a 54-inch eco solvent printing machine?

UM: Print width should follow your most common job size, not your wishful thinking about future jobs. A 64-inch machine costs more to buy, more to maintain, and wastes media if 80% of your work fits in 54 inches — but if vehicle wraps are a core service, the extra width isn’t optional, it’s essential. Map your actual order history before you spec the machine.

DTF

Textile Printing Machine Selection Roadmap: DTF, Sublimação, or Wide-Format Inkjet?

Understanding Your Textile Printing Machine Options: DTF vs Sublimation vs Wide-Format Inkjet Performance

OK so here’s the thing nobody tells you when you’re shopping for your first textile printer: the technology you pick matters way more than the brand name on the front. I learned this the hard way after spending six grand on a machine that was technically great but totally wrong for what I actually needed to print.

Direct-to-film (DTF) has basically taken over the custom apparel world in the last couple years — and for good reason. You print your design onto a special film, dust it with adhesive powder, cure it, then heat-press it onto pretty much any fabric. Algodão, poliéster, blends, even leather if you’re feeling adventurous. The initial investment runs anywhere from $3,000 to $15,000 depending on width and speed, but here’s what sold me: you can print white ink. Sounds simple, but that one feature opens up dark garments in a way other methods just can’t touch.

Sublimation is the other heavy hitter. Different beast entirely.

It only works on polyester or poly-coated surfaces (think mugs, phone cases, those weirdly popular car seat covers), but when it works, the colors are insane. Like, genuinely more vibrant than anything DTF can produce. The ink turns into gas under heat and bonds at a molecular level with the fabric — so it never cracks, never peels, never fades in the wash. But you’re locked into light-colored poly fabrics. That’s the trade-off.

Then there’s wide-format inkjet, which is basically a Graphic Printing Machine that someone convinced to print on fabric instead of vinyl banners. These things are massive (some hit 64 polegadas de largura), crazy fast, and they’ll handle soft signage, flags, backdrops, trade show graphics. Not really for t-shirts unless you’re doing all-over prints or cutting and sewing custom patterns. Think industrial scale — I’ve seen shops running 500-yard orders on these.

Each technology has its lane. DTF for custom apparel with no minimums. Sublimation for poly products with permanent, photo-quality color. Wide-format for big textile runs where speed matters more than garment versatility. Choose based on what you’re actually selling, not what sounds coolest.

Which Graphic Printing Machine Technology Actually Matches Your Production Volume and Fabric Types

I watched a startup blow $40,000 on a dye-sublimation setup last year because someone told them it was “the future of textile printing.” They were printing mostly cotton tees. Sublimation doesn’t work on cotton. At all. The machine sat there for three months before they sold it at a loss.

Impressoras eco solvente

So let’s talk real numbers and actual fabric compatibility, because the Graphic Printing Machine you pick needs to match what you’re physically printing — not what you think you might print someday.

DTG (direct-to-garment) handles low-to-medium volume really well. Estamos conversando 20-200 pieces per day if you’re running efficiently. Algodão, cotton blends, anything with natural fibers — DTG loves that stuff. Polyester? Not so much. The ink sits on top instead of bonding, and you get this weird plasticky feel. I’ve seen shops push 300 shirts in a day on a good industrial DTG unit, but you’re babysitting the thing constantly (white underbase clogs, print heads need cleaning, the usual drama). Best for on-demand operations or small custom runs where setup time matters more than raw speed.

Dye-sublimation is the opposite animal. High volume only makes sense here — you need at least 100-piece runs to justify the setup. But if you’re doing polyester all day (athletic wear, performance fabrics, promotional items), nothing touches it for permanence. The color literally becomes part of the fabric. I tested a sublimated jersey that went through 50 wash cycles with zero fade. Zero. A captura? Polyester only. Maybe poly-blends if you’re OK with muted colors on the natural fiber percentage.

Screen printing still wins for massive runs — 500+ pieces of the same design. Algodão, poly, blends, doesn’t matter much. And honestly, for simple 1-3 color jobs on heavy fabric like hoodies or canvas bags, nothing beats the durability. Setup time kills you on small orders, no entanto. Anything under 50 pieces and you’re losing money on labor.

Wide-format textile printers (the ones that look like they belong in a print shop, not a garment factory) are for soft signage, bandeiras, trade show backdrops — basically anything that’s fabric but not a garment. These run 100+ yards per hour on polyester or treated cotton. Not your tool for t-shirts unless you’re cutting and sewing custom patterns afterward.

Match the technology to your actual daily workload. Not your dream workload. Your actual orders from last month.

Real-World Cost Breakdown: Comparing Initial Investment and Per-Print Economics for DTF, Sublimação, and Inkjet Systems

I burned through $18,000 learning this the hard way, so let me save you the tuition.

Banner printing machine

DTF printers look cheap up front — you can get a decent A3 setup for around $4,500 — but the consumables will murder you if you’re not careful. Powder, film, ink, hot-melt adhesive sheets. I was paying $0.85 per print for an 11×15 transfer once you factor everything in. That’s before labor. The break-even point for me was around 40-50 shirts per design, which worked great for local sports teams but tanked my margins on custom one-offs. And the film waste? You’re throwing away at least 15% on trimming and failed prints while you dial in your settings.

Sublimation is the opposite math. Entry cost is lower — a solid 13-inch Sawgrass setup runs about $2,800 — and your per-print cost drops to maybe $0.30 for an average design (ink and paper, that’s it). But here’s the catch: polyester only. White polyester, ideally. I watched a friend buy a $12,000 wide-format sublimation printer for “custom activewear” and then realize 60% of his inquiries were for cotton hoodies. Expensive mistake.

Technology Initial Investment Cost Per Print (11×15) Break-Even Volume
DTF (A3 system) $4,500–$8,000 $0.75–$1.20 40–60 units/design
Sublimação (13″ impressora) $2,800–$5,500 $0.25–$0.45 20–30 units/design
Modified Inkjet (Epson ET-8550) $600–$1,200 $0.15–$0.30 10–20 units/design

Modified inkjet setups — basically hacking an Epson EcoTank with sublimation or pigment inks — are how most people actually start. Low upfront cost. Stupidly cheap per print. But you’re limited to 13×19 max, and if you’re running a graphic printing machine all day, the printheads will clog on you every 6-8 weeks (ask me how I know). Fine for side hustles. Not fine for production.

So calculate your monthly volume first, then work backward to the technology. Not the other way around.

Matching Textile Printing Machine Capabilities to Your Business Model — Custom Orders, High Volume, or Multi-Substrate Flexibility

I watched a guy drop $48,000 on a DTG flatbed last year because “it looked professional” — then realize three months later he was doing 90% custom tote bags and maybe 12 T-shirts a month. Wrong machine. Completely wrong.

Your business model dictates the tech stack, not the other way around. If you’re running a print-on-demand storefront with 200 SKUs and orders trickling in one or two at a time, you need a different textile printing machine than someone cranking out 500 identical hoodies for a corporate client. And both of those are wildly different from a contract printer doing fashion samples on silk one day and canvas totes the next.

Custom orders — the Etsy crowd, the wedding favor people, the guy who makes ironic dad hats — need speed-to-first-print and low setup waste. DTG wins here. You’re not doing prepress. You’re not mixing Pantone inks. You upload a file, hit print, cure it, done. A single-head DTG can handle 8–12 custom garments an hour if you’re moving. The per-unit cost sucks compared to screen printing, but setup time is zero, so your margins still work on one-offs.

High-volume shops — think merch for bands, company uniforms, bulk blanks for resellers — should be looking at automatic screen presses or hybrid UV-DTF systems. Once you’re past 50 units per design, screen printing demolishes everything on cost per piece. An 8-color auto can do 250+ shirts an hour. But setup takes 45 minutes and you’re eating the cost of screens, so anything under 24 units doesn’t pencil out. (I’ve seen shops refuse orders under 48 pieces for this exact reason.)

Multi-substrate flexibility is where it gets weird. If you’re printing on cotton e poliéster e madeira e ceramic — yeah, sublimation or a modded graphic printing machine with pigment inks is your only real play. You lose some color vibrancy on natural fibers, but you gain the ability to say yes to almost any substrate. A 13-inch sublimation printer with a heat press will handle fabric, canecas, mouse pads, and metal prints. Jack of all trades. Master of none — but sometimes that’s exactly what a startup needs.

Conclusão

Here’s the truth: most people overthink this decision. If you’re printing on cotton and doing small batches, DTG is still king. High volume on polyester blends? Screen or UV-DTF wins every time. The Textile Printing Machine that’s “best” is whichever one matches your actual order mix — not the one with the flashiest spec sheet.

I’ve watched shops drop $40K on equipment that sits idle because they chased capability instead of capacity. Start with your real numbers: what substrates are you actually printing on, what’s your average order size, and how fast do you need to scale. Those three answers will narrow your field to maybe two machines.

And if you’re still torn? Rent first. Most distributors offer 30-day trials now. Run your actual jobs through it before you sign anything.

Frequently Asked Questions

P: How much does a Textile Printing Machine actually cost?

UM: Entry-level DTG machines start around $15K (Epson F2100 territory), mid-range direct-to-film setups run $25K–$45K, and industrial screen printing automatics can hit $80K–$150K. The real cost isn’t the machine though — it’s the consumables, maintenance contracts, and whether you’re financing or paying cash. I’ve seen shops spend more on ink and pretreatment in year two than they did on the equipment itself.

P: What’s the difference between DTG and DTF printing?

UM: DTG (direct-to-garment) prints straight onto fabric using modified inkjet tech — think of it like a giant printer that eats t-shirts. DTF (direct-to-film) prints onto a special film first, then heat-transfers that image onto the garment. DTG gives you softer prints on cotton but needs pretreatment; DTF works on damn near anything (poliéster, nylon, couro) but feels slightly thicker.

P: Can I run a Textile Printing Machine from home?

UM: Technically yes, but your neighbors might hate you. Most machines need dedicated 220V power, proper ventilation (those fumes are no joke), and climate control — humidity kills print quality fast. I know three people running DTG setups in converted garages, and all of them wish they’d gone straight to a commercial space. The noise alone from a conveyor dryer will end friendships.

P: How long does it take to print one shirt?

UM: A DTG Textile Printing Machine takes 2–4 minutes per shirt depending on design complexity (full-color photorealistic images eat more time). Screen printing is way faster once you’re set up — maybe 20 seconds per piece — but setup eats an hour. UV-DTF is the sweet spot for speed: 30–45 seconds per transfer, no pretreatment needed.

P: What fabrics work best with textile printing machines?

UM: 100% cotton is still the gold standard for DTG — the ink bonds beautifully and the hand-feel stays soft. Poly-cotton blends (50/50 or 60/40) work but you’ll see some color shift and need white underbase. Straight polyester needs either sublimation equipment or DTF transfers; trying to DTG print on poly is like writing with a Sharpie on wax paper.

P: Is buying a used Textile Printing Machine worth the risk?

UM: Depends entirely on the print head hours and maintenance records. A two-year-old machine with 500 hours and documented cleaning logs? Solid deal at 40% off retail. A five-year-old unit with mystery service history and a “works great!” description on Facebook Marketplace? Pass — you’re buying someone else’s expensive problem. Always get a tech inspection before you wire money.

P: Why do some prints crack or fade after washing?

UM: Usually it’s a curing issue — you didn’t hit the right temperature long enough, or your conveyor dryer speed was too fast. Cheap ink matters too (I learned this the expensive way with a bulk supplier in 2026). The other culprit is fabric prep: oil, sizing chemicals, or fabric softener residue will wreck ink adhesion no matter how perfect your Textile Printing Machine settings are.

Impressora jato de tinta

O que uma grande impressora jato de tinta realmente faz (E por que as especificações são mais importantes do que a marca)

A maioria dos compradores se fixa primeiro nos nomes das marcas. Esse é o ponto de partida errado.

UM large inkjet printer works by propelling microscopic droplets of ink — sometimes as small as 2 picolitros – através de um cabeçote de impressão e em um substrato com precisão suficiente para reter linhas finas, gradientes, e detalhes fotográficos em larguras que uma máquina desktop não poderia alcançar. Estamos conversando 24 polegadas, 44 polegadas, 60 polegadas de largura. Alguns sistemas alimentados por rolo vão ainda mais longe. A tecnologia principal parece bastante simples, mas as variáveis ​​abaixo dessa descrição básica são onde os compradores consistentemente se queimam: tamanho da gota, configuração do cabeçote de impressão, química da tinta, manipulação de mídia, e o método de secagem interagem de maneiras que as folhas de especificações nem sempre explicam claramente.

Então, aqui está a questão das especificações: elas não são apenas números para impressionar você em uma feira comercial. UM commercial inkjet printer running aqueous dye inks will produce stunning color on coated photo paper and look completely washed out on uncoated banner material. Swap to a solvent or latex ink system and suddenly you’ve got outdoor durability, but your fine-art reproduction quality takes a hit. Neither is universally better. It depends entirely on what you’re printing, how often, and on what surface.

And the “large plotter printer” category specifically adds another layer of complexity — these machines are built around precision drafting and technical output, where dimensional accuracy matters more than color gamut. An architectural firm printing CAD drawings has almost nothing in common with a print shop running retail signage, even if both are using a 36-inch wide-format machine from the same product family.

The table below breaks down the primary spec categories that actually affect real-world output quality — not the marketing highlights, but the functional differences worth comparing before you commit to a purchase:

Spec CategoryWhy It MattersWhat to Look For
Print Resolution (DPI)Determines fine detail and edge sharpness1200 DPI minimum for photo/graphic work
Ink TypeAffects durability, color range, and media compatibilityMatch ink chemistry to your primary substrate
Printhead TechnologyImpacts speed, consistency, and maintenance costPiezo vs. thermal — piezo tends to last longer
Max Print WidthSets the ceiling on your output format optionsBuy wider than your current largest job requires
Media HandlingDetermines substrate flexibility and workflow speedRoll-to-roll vs. flatbed vs. hybrid configurations

Print Width, Resolution, and Ink Systems — The Three Numbers You Can’t Ignore

Three numbers. That’s really what separates a machine that fits your operation from one that becomes an expensive paperweight six months in. Print width, resolution, and ink system — get all three right, and almost everything else is just fine-tuning.

Print width is the obvious one, but buyers consistently underestimate it. The rule of thumb that actually holds up in practice: buy wider than your biggest current job demands. If your largest regular output is 42 polegadas, look at a 54- or 60-inch machine. Why? Because the moment you start turning away a client because your large inkjet printer can’t physically fit their banner, you’ve already lost more than the machine’s cost differential. A large plotter printer running at 60 inches doesn’t cost dramatically more to operate than a 44-inch model — but the ceiling it removes from your revenue potential is significant.

Resolution is where people get tangled up in specs that don’t always translate to real-world results. Honest answer: 1200 DPI is a reasonable floor for graphics and photo work, but the printhead technology matters just as much as the number itself. A machine printing at 1200 DPI with a well-calibrated piezo head — Epson’s PrecisionCore architecture is a good reference point here — will outperform a thermal system rated at 2400 DPI that’s running with clogged nozzles. So don’t chase the bigger number blindly.

Ink chemistry is where things get genuinely complicated (and where a lot of buyers make expensive mistakes). Aqueous inks are excellent for indoor photo and fine art output but will fade or bleed on outdoor substrates. UV-curable inks adhere to rigid materials — acrylic, aluminum composite, foam board — and cure instantly under UV lamps, which speeds up workflow considerably. Solvent and eco-solvent inks sit somewhere in the middle: outdoor-durable, flexible enough for vehicle wraps, and compatible with a wide range of vinyl media. Any commercial inkjet printer running outdoor signage or fleet graphics work almost certainly needs solvent or UV capability.

Match the ink system to your primary substrate first. Everything else follows from that decision.

Impressora jato de tinta

Where a Large Plotter Printer Fits vs. Where It Doesn’t

Fit matters more than features. A large plotter printer sitting in the wrong environment is just an expensive dust collector — and that’s not an exaggeration if you’re a small print shop running maybe 10-15 wide-format jobs a week on a machine built for 10x that volume.

So where does a large inkjet printer genuinely earn its keep? Commercial print shops, architectural firms, interior design studios, event production companies, and any operation doing consistent wide-format output at scale. These are environments where the throughput justifies the footprint, the maintenance overhead, and the media costs. A commercial inkjet printer running at near-capacity is a completely different value proposition than one sitting idle three days out of five.

Not every buyer fits that profile, no entanto.

A freelance photographer who occasionally prints exhibition pieces doesn’t need a 64-inch roll-fed beast — a desktop photo printer at a fraction of the cost handles that workload without the ink maintenance headaches that come with machines left idle for extended periods (and yes, clogged heads are a real operational cost, not just an inconvenience). Same logic applies to small marketing teams who send maybe two or three banner jobs a year to an outside vendor. Outsourcing those runs is almost always cheaper than ownership when volume is that low.

But when volume crosses a certain threshold — say, daily print runs, consistent substrate variety, or tight turnaround requirements — in-house wide-format production starts making serious financial sense. Buyers sourcing through suppliers like SINOTEC often hit this crossover point when they’re scaling a regional print operation or building out commercial production capacity for OEM or contract work.

  • High fit: print shops, trade show producers, empresas de sinalização, architectural visualization studios
  • Low fit: occasional-use creative freelancers, small offices with minimal visual output needs
  • Gray zone: mid-size marketing departments — depends entirely on monthly print volume and turnaround sensitivity

Honest answer? Most buyers overestimate their volume and underestimate their maintenance commitment. Know your actual monthly square footage before you commit to anything.

Impressora jato de tinta

How to Match a Commercial Inkjet Printer to Your Real-World Output Needs

Matching the machine to the actual job — not the job you imagine you’ll have six months from now — is where most buyers go wrong. The spec sheet looks great. The demo print looks great. And then the printer sits at 40% utilization because the workload never materialized the way the purchase justification said it would.

So here’s a more grounded way to think about it. Start with your dominant output type, not your maximum output type. A commercial inkjet printer built around textile or backlit film production has a completely different ink system and media handling setup than one optimized for CAD drawings or technical schematics. These aren’t interchangeable — not without real performance trade-offs.

Three variables actually matter most when you’re trying to match a large inkjet printer to real commercial workloads:

  • Media range — how many substrate types does your operation actually run per month? (If the honest answer is “mostly one or two,” you don’t need a hybrid machine.)
  • Speed vs. quality balance — production signage can tolerate faster, lower-pass printing; fine art reproduction or architectural rendering cannot
  • Ink system durability — pigment-based systems hold up better for outdoor applications; dye-based systems punch harder on color gamut for indoor display work

A large plotter printer in a high-volume technical environment — think engineering firms running daily blueprint output — has almost nothing in common with a wide-format unit serving a trade show graphics shop, even if both machines print at 60 polegadas de largura. Same category. Completely different animal.

Buyers sourcing at scale, particularly those working with OEM-focused suppliers on customized builds, often find that nailing the ink system first simplifies every other decision downstream. Get that wrong and you’re fighting the machine on every job.

Not complicated. Just specific. The buyers who get this right are the ones who audit their actual job logs — real substrate types, real turnaround windows, real monthly square footage — before they ever open a product catalog.

Conclusão

The spec sheet is not your friend here. What actually matters — ink system, substrate range, real duty cycle — lives in your own job logs, not in a manufacturer’s marketing copy.

Buying a large inkjet printer without auditing your actual workload first is how businesses end up with expensive hardware that fights them on every run. Pigment or dye, roll-fed or flatbed, 44-inch or 64-inch — none of those calls are hard once you know what you’re genuinely printing, how often, and on what.

Get specific before you get shopping.

Frequently Asked Questions

P: What is a large inkjet printer actually used for in a commercial setting?

UM: Large inkjet printers handle output that desktop units can’t — think banners, trade show graphics, envelopamento de veículos, architectural drawings, fine art reproductions, and wide-format photography. The defining factor is print width, typically 24 inches and up, which is what separates them from standard office hardware. Most commercial buyers are running roll media, though flatbed configurations handle rigid substrates like foam board, acrílico, and aluminum composite.

P: How much does a large inkjet printer cost?

UM: Entry-level wide-format machines from brands like Epson or Canon start around $1,500–$3,000 for 24-inch models, but production-grade large inkjet printers — 44-inch to 64-inch roll-fed units — run $10,000 to $30,000+. Flatbed UV systems can push past $80,000 depending on bed size and ink configuration. The hardware price is only part of it; ink, media, and maintenance contracts stack up fast.

P: What’s the difference between pigment and dye ink in a large inkjet printer?

UM: Pigment ink sits on top of the substrate and resists UV fading — it’s what you want for outdoor signage or archival prints. Dye ink absorbs into the media and produces more vibrant color on coated papers, but it fades faster under direct light. Choosing the wrong ink system for your primary use case is one of the most expensive mistakes buyers make.

P: How long do large inkjet prints actually last outdoors?

UM: Unlaminated outdoor prints using quality pigment ink typically hold for 1–3 years under direct sun exposure. Add a UV-resistant laminate and that number climbs to 5–7 years on most vinyl substrates. Dye-based output degrades significantly faster — sometimes within months in high-UV environments — which is why substrate and ink pairing matters before you quote a client on durability.

P: Can a large inkjet printer handle rigid materials like wood or metal?

UM: Roll-fed printers can’t — that’s a flatbed UV inkjet job. Flatbed large inkjet printers use UV-curable ink that bonds directly to rigid surfaces including aluminum, vidro, madeira, ceramic tile, and even some plastics. If rigid media is a core part of your workload, a hybrid flatbed (which handles both roll and rigid) is worth the premium over a roll-only unit.

P: Why do large inkjet printers have such high running costs?

UM: Ink is the main culprit — wide-format machines consume it fast, and OEM cartridges aren’t cheap. A 64-inch production printer running full-coverage graphics can burn through hundreds of dollars in ink per day at volume. Add printhead maintenance, waste ink tanks, and media costs, and your cost-per-square-foot calculation looks very different from the spec sheet’s headline number. Buyers sourcing through OEM/ODM channels — suppliers like SINOTEC that work directly with manufacturers — sometimes find better ink pricing on compatible systems without sacrificing output quality.

P: How do I know what size large inkjet printer I actually need?

UM: Pull your last three months of job logs and find your most common output width — then buy one size up from that. Most shops think they need a 64-inch machine when a 44-inch unit would handle 90% of their actual volume with lower media waste and faster pass speeds. Overbuying on width is a real thing, and it costs you in media costs on every job that doesn’t fill the bed.

P: Is it worth buying a used large inkjet printer instead of new?

UM: It depends almost entirely on the printhead hours — that’s the number sellers don’t always volunteer. A used large inkjet printer with low head hours and documented maintenance can be a solid buy at 40–60% off retail. Skip anything with no service history, clogged heads, or a discontinued ink system; the repair and consumables situation turns ugly fast, and manufacturer support on discontinued models is essentially nonexistent.

DTF

Como a sublimação e a impressão DTF realmente funcionam – e por que a diferença é importante

Sublimação e DTF não são a mesma coisa – e confundi-los custará dinheiro, tempo, e uma pilha de espaços em branco arruinados. Então, vamos detalhar o que está acontecendo dentro de cada processo, porque a química é mais importante do que a maioria das pessoas imagina.

UM sublimation printer works by converting solid dye into gas under heat — skipping the liquid phase entirely. Esse gás se liga diretamente às fibras de poliéster (ou superfícies duras revestidas com polímero) em torno de 375–400°F, tornando-se parte do próprio material. Não sentado em cima. Dentro dele. É por isso que as impressões por sublimação não parecem nada quando você as toca – não há camada de tinta para descascar ou rachar. A captura? Só funciona em cores claras, substratos pesados ​​em poliéster. Algodão? Esqueça. UM 100% camiseta de algodão lhe dará o fantasma desbotado de uma imagem, não é uma impressão vibrante.

DTF — direto para filme — funciona de maneira completamente diferente. UM DTF garment printer deposits ink onto a special film, espana com pó adesivo termofusível, cura isso, then transfers the whole thing onto fabric using a heat press. It sticks to almost anything: cotton, blends, dark fabrics, textured surfaces. That flexibility is genuinely useful. But the transfer layer sits on top of the fabric, and you can feel it — some buyers love the texture, others don’t.

Here’s where it gets interesting for product diversification. The same thermal-transfer logic that drives garment printing shows up in completely different market segments. How a Phone Case Printer Vending machine operates — heating a pre-printed film onto a case shell — borrows from the same fundamental transfer mechanics. And the conversation around Phone Case Printer Vending Machine vs. traditional retail setups often comes down to exactly this: transfer quality and substrate compatibility. How Countries Embrace Phone Case Printer technology also varies wildly — markets in Southeast Asia lean toward high-volume vending kiosks, while European buyers often prioritize print durability specs. Top Spots for Profitable Phone Case printing operations tend to cluster around high foot traffic and customization demand, not just equipment cost.

For straight garment work, um sublimation t shirt printer dominates when you’re running polyester sportswear or branded merch at scale. Soft hand-feel, zero cracking, wash durability that actually holds up past 50 cycles. Suppliers like SINOTEC who handle OEM spec work for international buyers see this distinction constantly — clients ordering sublimation setups for activewear and DTF rigs for fashion blanks. Different tools. Different jobs. Neither one is universally better.

Pick the wrong process and you’re not just wasting supplies. You’re reprinting entire runs.

The Sublimation T-Shirt Printer: What It Does Well and Where It Hits a Wall

Polyester is where a sublimation t shirt printer is basically unbeatable. Full stop. The dye bonds at a molecular level with the fabric — not sitting on top of it, not cracking off after a dozen washes — and the result is a print that genuinely outlasts the shirt itself in most cases. Sportswear brands, team kits, branded activewear runs: this is the machine’s home territory, and it owns it.

But here’s the wall, and it’s a hard one. Natural fibers. Algodão, linen, bamboo blends — sublimation dye has almost nothing to bond with on those materials, so the color either fades fast or never saturates properly to begin with. A DTF garment printer sidesteps that problem entirely by applying a film transfer that sticks regardless of fiber content, which is exactly why fashion-forward buyers running cotton streetwear blanks keep landing on DTF setups instead. Different chemistry. Different use case.

The substrate limitation trips up a lot of first-time buyers who see the print quality on a polyester sample and assume it’ll translate to everything in their catalog. It won’t. (This is also why understanding your actual product mix before buying any equipment matters more than any spec sheet comparison.)

There are also considerations beyond the garment itself. How a Phone Case Printer Vending operation handles substrate diversity is actually a useful comparison point here — those machines are engineered around a fixed substrate, which is why they work so cleanly. A sublimation printer runs best when you’ve similarly locked down your material choices. Versatility isn’t really the pitch. Consistency is.

  • Polyester and poly-blend fabrics: excellent color saturation, wash durability past 50+ cycles
  • Cotton and natural fibers: poor dye bonding, not recommended without a polymer coating pre-treatment
  • Hard substrates (canecas, panels, cases): works well with the right heat press setup
  • White or very light base colors required — sublimation can’t print on dark fabric effectively

So the honest summary is this: a sublimation printer is a precision tool, not a catch-all. Know your substrate. Know your volume. Buy accordingly.

DTF garment printer

The DTF Garment Printer: Broader Fabric Range, Different Trade-Offs

DTF — direct-to-film — solves the problem that sublimation simply can’t. Dark fabrics. Algodão. Textured blends. All the stuff that sends a sublimation t shirt printer sideways is basically fair game for DTF, because the process works differently at a fundamental level: ink gets printed onto a release film, a hot-melt adhesive powder gets applied, the film cures, and then the whole transfer gets heat-pressed onto the garment. No dye migration. No substrate dependency. Just ink sitting on top of the fabric, bonded through adhesive.

That’s genuinely useful. But it comes with trade-offs that buyers routinely underestimate.

The feel is different — a DTF transfer has a slight hand to it, a texture you can run your finger across. On a premium cotton tee it’s usually fine. On athletic polyester that needs to breathe and flex? It can feel restrictive, especially on larger prints. And wash durability, while solid in the 30–40 cycle range for quality transfers, doesn’t quite match what a good sublimation setup delivers on poly fabric. The dye-bonded-into-fiber result of sublimation just ages more gracefully on the right substrate.

So what’s the DTF garment printer actually good for? Honestly, short runs on mixed fabrics. Custom one-offs. Shops that can’t afford to tell customers “sorry, we only do light-colored polyester.” The flexibility is the product.

There’s also a cost-per-print reality worth flagging (especially for anyone running volume). DTF film, powder, and ink together add up faster than sublimation consumables at scale. For a high-output operation printing hundreds of identical polyester jerseys, sublimation wins on economics. For a shop doing 10-unit mixed orders every week, DTF makes more sense operationally.

  • Works on cotton, dark fabrics, and blended materials — sublimation cannot
  • Slight surface texture on finished prints; more noticeable on stretch fabrics
  • Wash durability: strong, but typically trails sublimation-on-poly over 50+ cycles
  • Higher consumable cost per print at volume
  • No base color restriction — dark garments are fine

And for context: suppliers like SINOTEC who handle commercial-grade digital print equipment see both technologies move steadily — which tells you neither has “won.” They serve different buyers with different constraints.

DTF garment printer

Sublimation Printer vs. Impressora DTF: Matching the Right Technology to Your Production Goals

OK so here’s the honest framing nobody gives you upfront: choosing between a sublimation printer and a DTF garment printer is less about which technology is “better” and almost entirely about what your order book actually looks like week to week.

Production volume changes everything. A sublimation t shirt printer running polyester blanks at scale — think 200+ units of the same design — delivers cost-per-print economics that DTF simply can’t touch at that quantity. The ink bonds into the fiber itself, so there’s no film layer, no texture, no peel risk after 60 wash cycles. But drop that same sublimation setup in front of a cotton tee or a dark-colored garment, and you’ve got a problem. It just doesn’t work.

Not a workaround problem. A physics problem.

DTF flips the constraint. It handles cotton, darks, blends — materials that sublimation ignores entirely — which is why retail customization shops tend to lean toward it. The tradeoff is consumable cost at volume and a slight surface texture that’s noticeable on stretch fabrics (athletes notice it; casual buyers usually don’t). So the math only tips toward DTF when your orders are mixed, short-run, or fabric-diverse.

And this is where it gets interesting for anyone thinking beyond garments. The same decision logic applies to adjacent markets — how a phone case printer vending setup gets specified, for instance, or how phone case printer vending machine vs. traditional retail kiosk models get evaluated by operators. Sublimation dominates phone case printing because the substrates are polymer-coated and the output is flawless. Understanding how countries embrace phone case printer deployments in high-traffic retail shows the same pattern: sublimation where the substrate cooperates, UV or DTF where it doesn’t.

Top spots for profitable phone case customization — airports, malls, tourist districts — almost universally run sublimation-based equipment. That’s not coincidence.

FactorImpressora de sublimaçãoDTF Garment Printer
Fabric compatibilityPolyester, polymer-coated onlyAlgodão, blends, dark fabrics
Best order sizeHigh-volume, uniform runsShort-run, mixed orders
Wash durabilityExcellent (50+ cycles)Strong, slightly lower
Consumable cost at volumeLowerHigher
Surface feelNo texture — ink is in the fiberSlight film texture

Conclusão

The substrate question settles everything. If your production runs polyester blanks or polymer-coated cases at any real volume, a sublimation printer earns its place fast — lower consumable costs, zero surface texture, and wash durability that holds up past 50 cycles. That’s a hard combination to beat.

Cotton-heavy catalog? Mixed short runs? Go DTF and don’t look back.

But if your substrate list cooperates, don’t overthink it. The high-traffic retail spots running sublimation equipment aren’t doing it by accident — they’re doing it because the math works, the output is clean, and the repeat order economics make sense at scale.

Frequently Asked Questions

P: What is a sublimation printer and how does it actually work?

UM: A sublimation printer uses heat to convert solid dye into gas — skipping the liquid phase entirely — which then bonds directly into the surface of a polymer-coated or polyester substrate. The result is ink that’s technically inside the material, not sitting on top of it, which is why the surface feels completely smooth and the color doesn’t crack or peel.

P: What materials can a sublimation printer print on?

UM: Polyester fabric and polymer-coated hard substrates are your lanes — think mugs with a polymer coating, phone cases, aluminum panels, and polyester jerseys. Cotton won’t work; the dye has nothing to bond to and you’ll get a faded, washed-out result that looks terrible after one cycle in the wash. Stick to substrates with at least 65% polyester content for fabric, and look for “sublimation ready” labeling on hard goods.

P: How much does a sublimation printer cost?

UM: Entry-level desktop units — like the Epson EcoTank converted setups or the Sawgrass Virtuoso SG500 — run between $300 e $600. Wide-format production sublimation printers (think 44-inch roll-fed machines from Epson or Mimaki) jump to $3,000–$15,000+ depending on throughput. For commercial buyers sourcing OEM-configured units through suppliers like SINOTEC, per-unit pricing on bulk orders can shift the economics significantly compared to retail channels.

P: Why does my sublimation printer produce faded or dull colors?

UM: Nine times out of ten it’s a temperature or time issue at the heat press — sublimation needs 375–400°F for most substrates, and even 10 degrees low will kill your vibrancy. Wrong substrate is the other culprit; if the material isn’t polyester or polymer-coated, the dye has nowhere to bond and the color just sits on the surface weakly before fading. Also check your ICC color profiles — printing without the right profile for your specific paper and ink combination will throw off your output every time.

P: How long do sublimation prints actually last?

UM: On polyester garments, a properly done sublimation print holds up well past 50 wash cycles without noticeable fading — that’s one of its biggest advantages over screen printing at volume. Hard substrate prints (canecas, panels) are essentially permanent under normal use. UV exposure is the real enemy outdoors, so for signage or outdoor apparel, factor in a UV-protective laminate or coating.

P: Can I use a regular inkjet printer for sublimation?

UM: Some Epson EcoTank models (the ET-2800 series, for example) can be converted using third-party sublimation ink — but you’re voiding your warranty and the results vary enough that it’s not a reliable production setup. A purpose-built sublimation printer uses printheads and ink delivery systems calibrated for sublimation dye, which means more consistent output and fewer clogging headaches. For anything beyond hobby-level runs, the converted inkjet route gets expensive in wasted transfers fast.

P: Is a sublimation printer worth it for small businesses?

UM: If your product catalog is polyester-heavy — custom sportswear, branded merchandise, personalized home goods — the consumable cost per print is low enough that a sublimation printer pays for itself quicker than most people expect. The math gets harder if you’re running mixed-substrate orders with a lot of cotton, because you’ll need a second printing solution anyway. Honestly, the businesses that struggle with sublimation ROI are usually the ones who bought the printer before locking down a consistent substrate lineup.

P: How do I stop my sublimation prints from ghosting?

UM: Ghosting happens when the transfer paper shifts slightly during or after pressing — even a millimeter of movement while the substrate is still hot creates a blurry double-image effect. Use heat-resistant tape to anchor all four corners of the transfer before pressing, and don’t peel the paper until the substrate has cooled enough that the dye is fully set. A quality heat press with even platen pressure helps too; uneven pressure is a ghosting accelerator that people underestimate.